EN
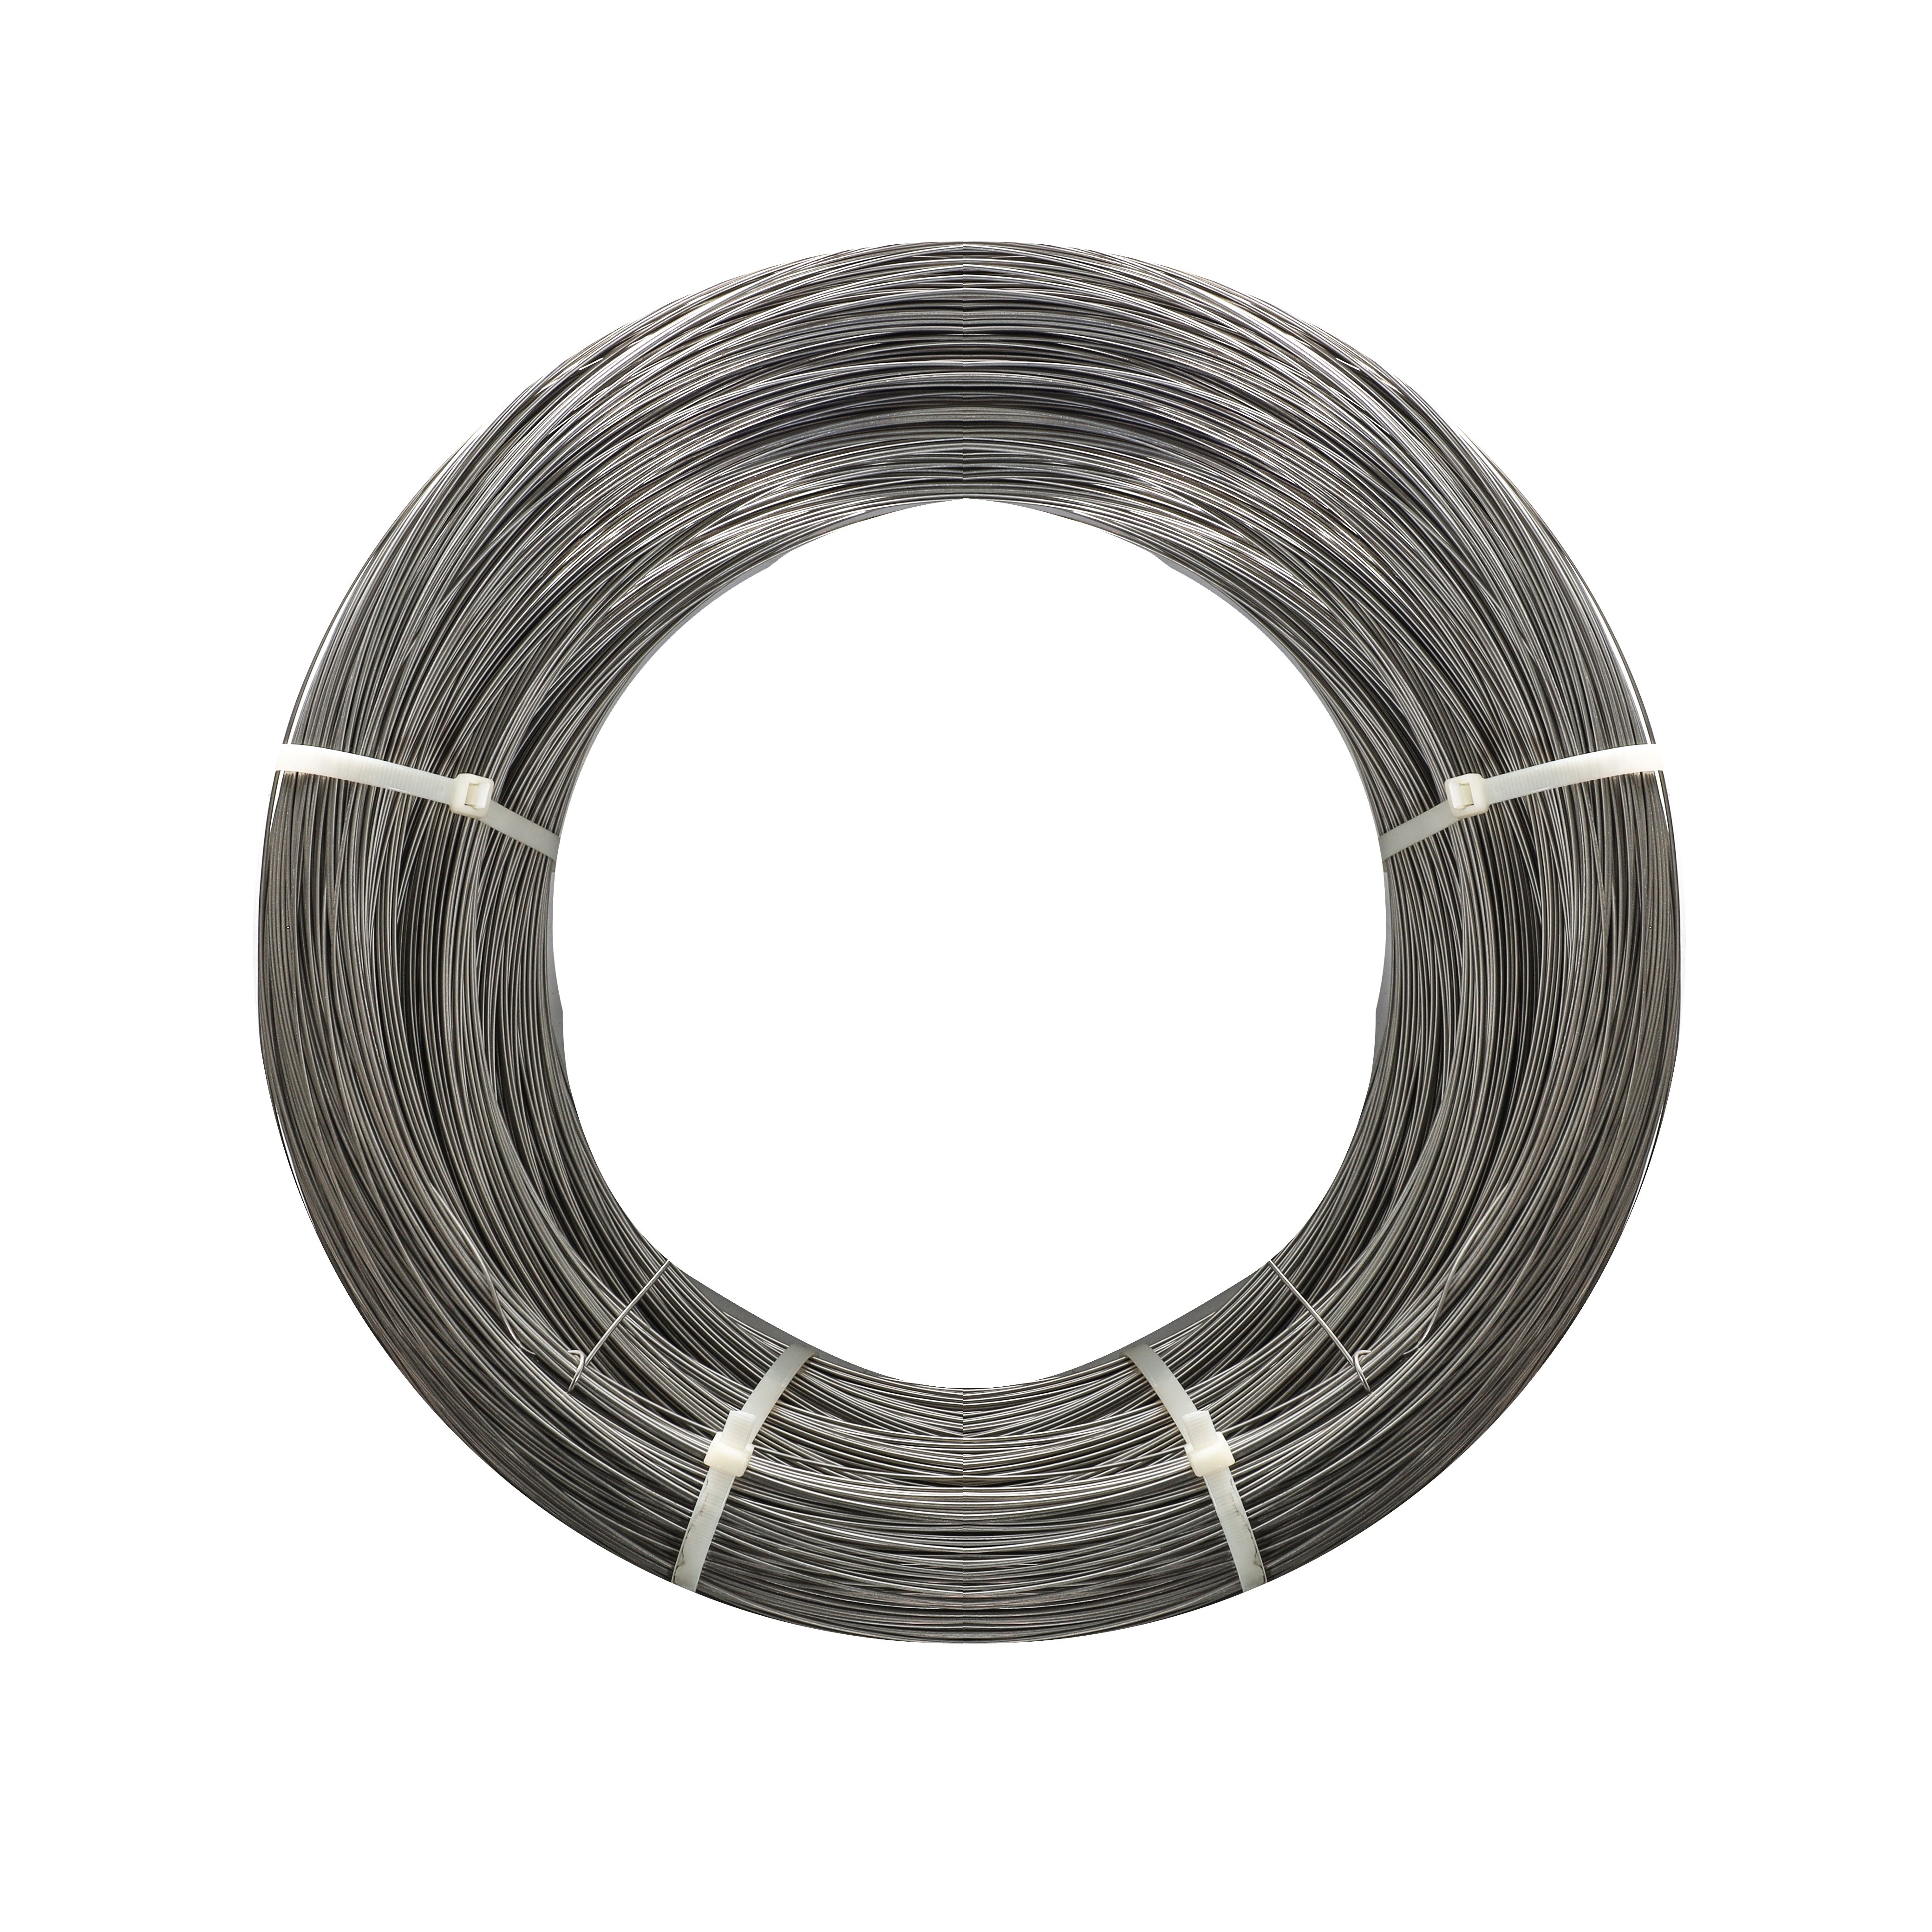
Precision Incoloy 800HT Cold Drawn Coil Wire 0.8-5.0mm for High-Temp Fasteners
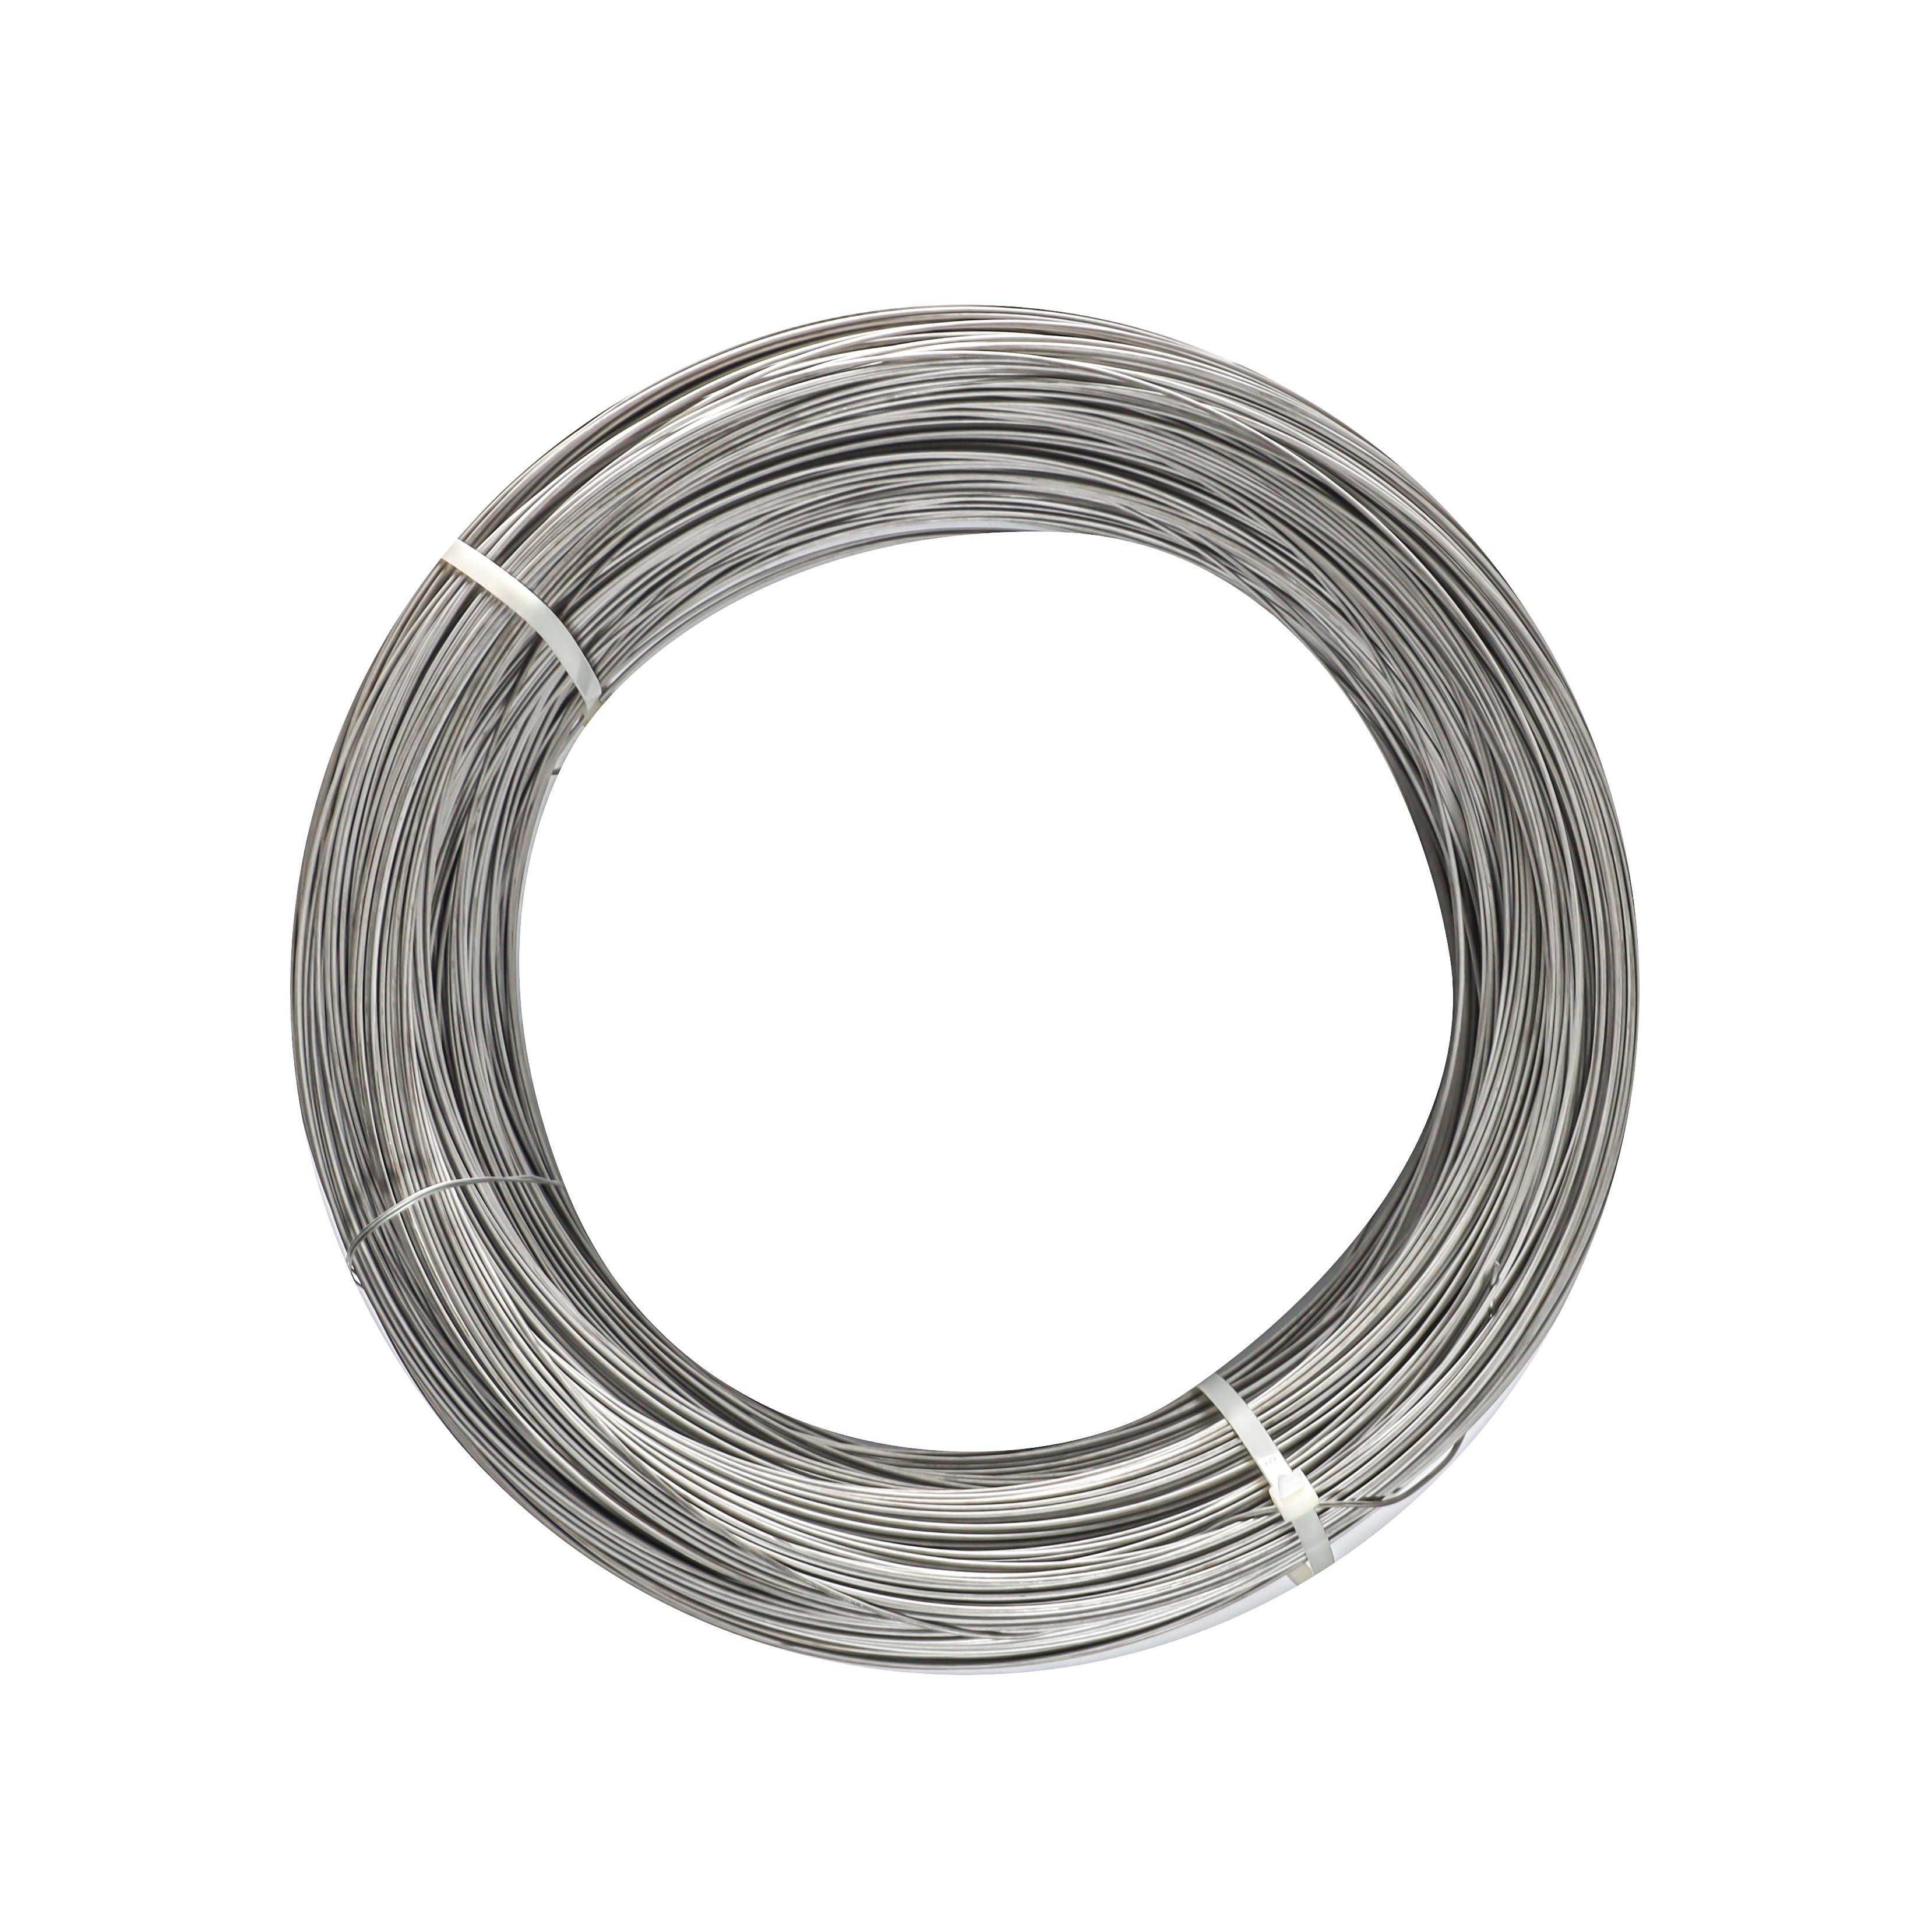
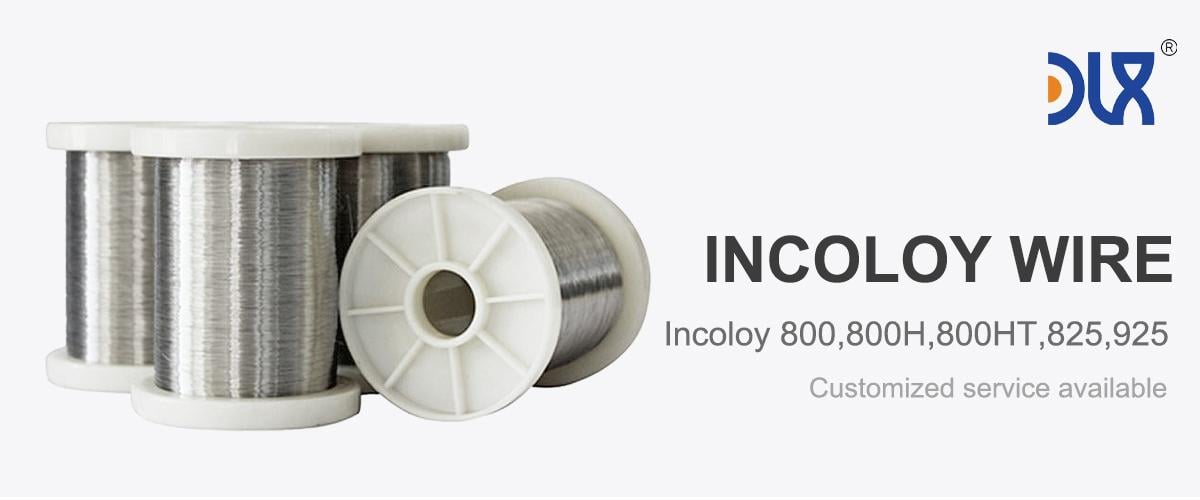
Engineered for demanding thermal environments, our Incoloy 800HT (UNS N08811) cold drawn coil wire in diameters from 0.8mm to 5.0mm provides exceptional high-temperature strength, oxidation resistance, and superior cold heading performance for industrial fastener fabrication.
- Overview
- Properties
- Advantages
- Applications
- Why-Us
- FAQ
- Recommended Products
Product Overview
UNS N08811 Nickel-Iron-Chromium Alloy for High-Stress Fasteners
Incoloy 800HT (UNS N08811) is a controlled-chemistry modification of standard iron-nickel-chromium alloys, engineered with strictly regulated carbon content and a precise cumulative titanium-plus-aluminum balance. This metallurgical design guarantees a stable, coarse-grained austenitic matrix that delivers exceptional creep-rupture strength and high structural integrity under continuous thermal loading.
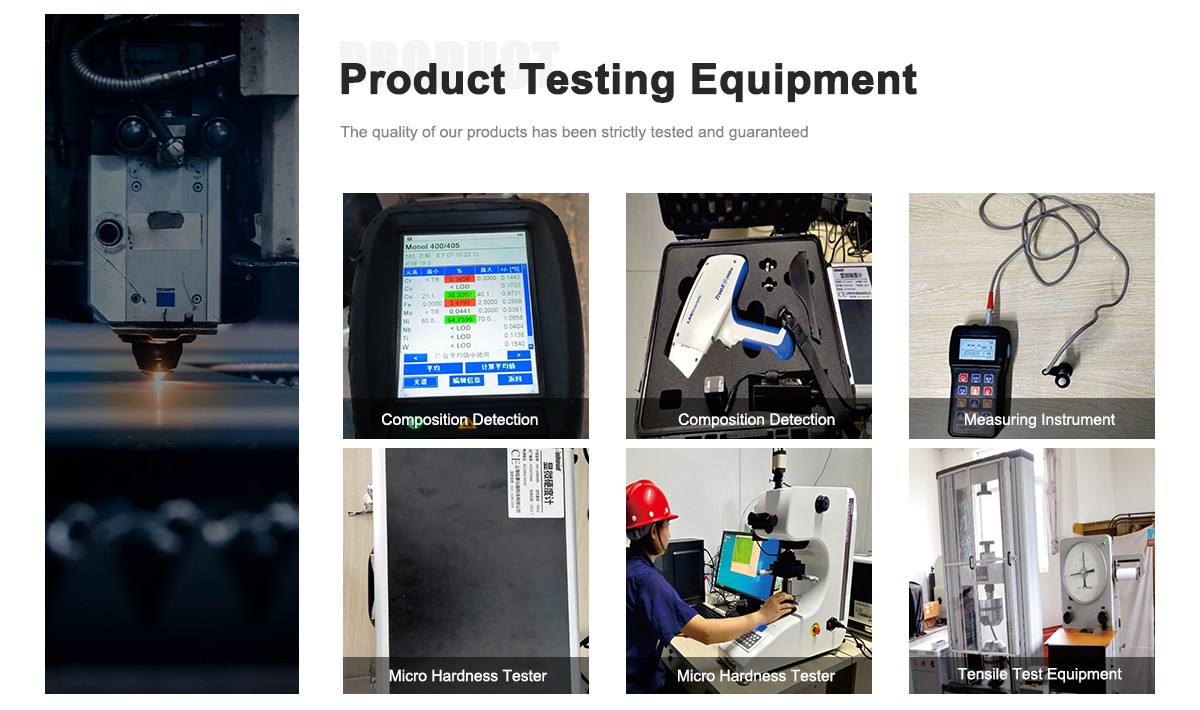
When processed into cold-drawn coil form, the wire undergoes uniform annealing and precision sizing to ensure homogeneous grain structure from coil core to surface. This eliminates micro-cracking risks during rapid automated cold heading, thread rolling, and hot upsetting operations.
Chemical Composition Window (%)
| Element | Content (%) | Metallurgical Function |
|---|---|---|
| Nickel (Ni) | 30.00 – 35.00 | Stabilizes austenitic structure; resists stress corrosion cracking |
| Chromium (Cr) | 19.00 – 23.00 | Forms protective oxide scale for high-temperature oxidation/carburization resistance |
| Iron (Fe) | Balance (≥ 39.50) | Matrix base balance |
| Carbon (C) | 0.06 – 0.10 | Regulates high-temperature creep strength and stability |
| Aluminum (Al) | 0.15 – 0.60 | Precipitates strengthening phases with Titanium |
| Titanium (Ti) | 0.15 – 0.60 | High-temperature structural stability |
| Al + Ti (Combined) | 0.85 – 1.20 | Optimized threshold for elevated temperature creep-rupture performance |
| Manganese (Mn) | ≤ 1.50 | Deoxidation and workability enhancement |
| Silicon (Si) | ≤ 1.00 | Surface scale adhesion and furnace resistance |
| Copper (Cu) | ≤ 0.75 | Residual control |
| Sulfur (S) / Phosphorus (P) | ≤ 0.015 each | Ultra-low trace impurities to prevent hot shortness |
Key Technical Properties
Creep Rupture Strength and Thermal Stability
1. Physical & Mechanical Performance Reference
-
Density: 7.94 g/cm³
-
Melting Range: 1357°C – 1385°C (2475°F – 2525°F)
-
Tensile Strength (Annealed/Drawn Condition): 550 – 750 MPa
-
Yield Strength (0.2% Offset): 220 – 450 MPa
-
Elongation at Break (A5): ≥ 30% – 42%
-
Elevated Temperature Stability: Continuous service capability up to 1000°C (1832°F)
-
Creep Rupture Threshold: Enhanced rupture endurance at sustained temperatures above 600°C
2. Dimensional Tolerances & Supply Scope
-
Diameter Range: 0.80 mm to 5.00 mm (Custom exact diameters available within 0.01mm increments)
-
Diameter Tolerance: Tight precision tolerance within ±0.015 mm to ±0.025 mm
-
Ovality (Out-of-Round): ≤ 50% of the total diameter tolerance
-
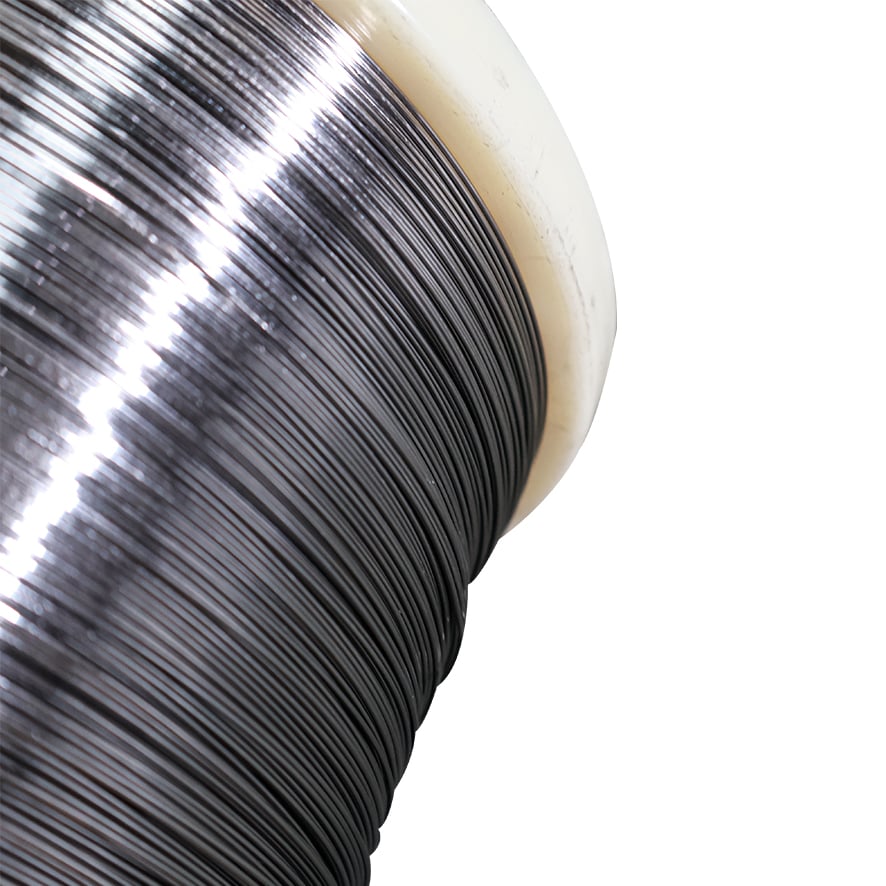
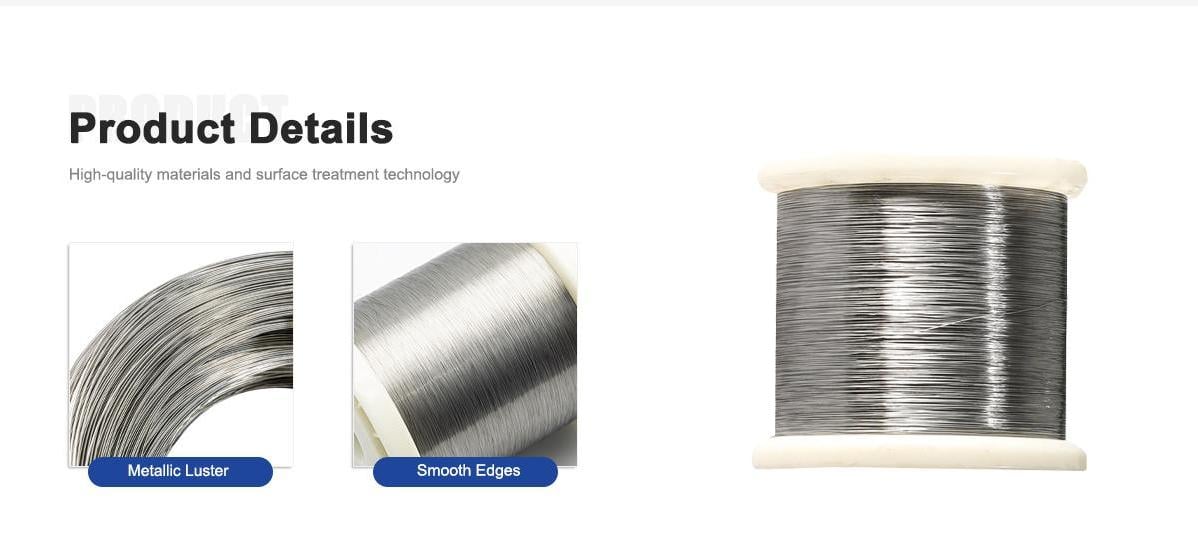
Surface Condition: Bright Annealed (BA), Acid Pickled, or Lightly Lubricated for Cold Heading Tool Protection
Manufacturing Advantages
Cold Heading and Thread Rolling Ductility
-
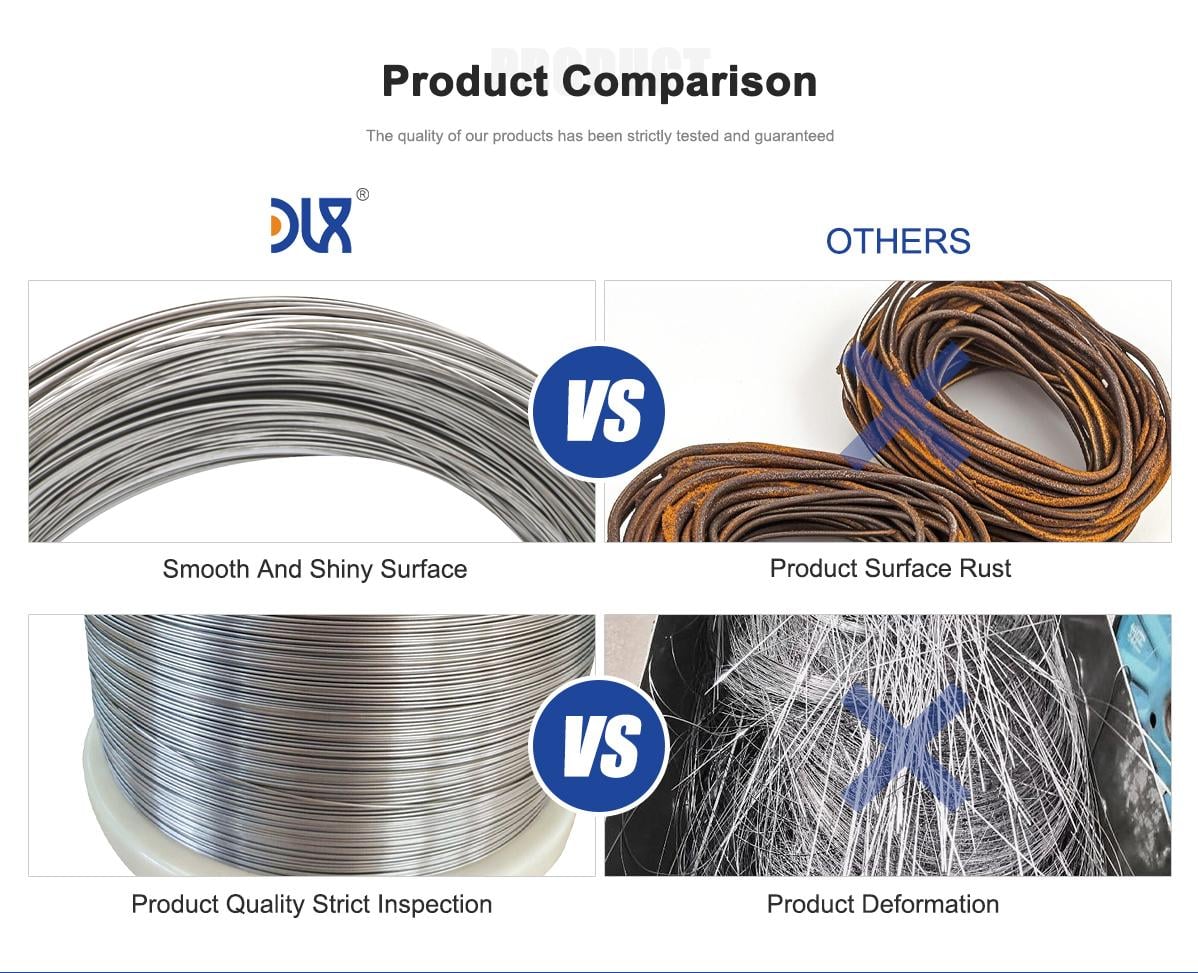
Superior Cold Heading Formability: Balanced annealing ensures high plasticity, preventing head cracking, shear bursts, or shank deformation during multi-station cold heading.
-
Flawless Thread Rolling Performance: Consistent cross-sectional tensile strength and minimal work-hardening gradients ensure clean, continuous thread profiles without surface laps or micro-fissures.
-
Uniform Grain Structure: Coarse-grain thermal processing ensures isotropic mechanical properties throughout the entire coil length, maximizing tooling life and minimizing production downtime.
-
Strict Surface Integrity: 100% eddy current surface defect testing and precision descaling eliminate seam lines, pits, and scratches.
Core Industrial Applications
High Temperature Fastener Manufacturing and Thermal Processing
-
Industrial Fasteners & Hardware: High-temperature studs, hex bolts, heavy-duty nuts, socket head cap screws, threaded rods, and retaining clips for extreme environments.
-
Petrochemical & Refining Equipment: Fastening hardware for ethylene cracking tubes, reforming furnaces, hydroprocessing units, and thermal piping flanges.
-
Power Generation & Boilers: Structural fasteners in superheater headers, steam turbine insulation jackets, and waste heat recovery systems.
-
Thermal Processing Furnaces: Baskets, fixtures, heating element pins, and hanger bolts inside continuous annealing and carburizing furnaces.
Why Choose DLX
Reliable Factory Direct Supply and Custom Coil Packaging
-
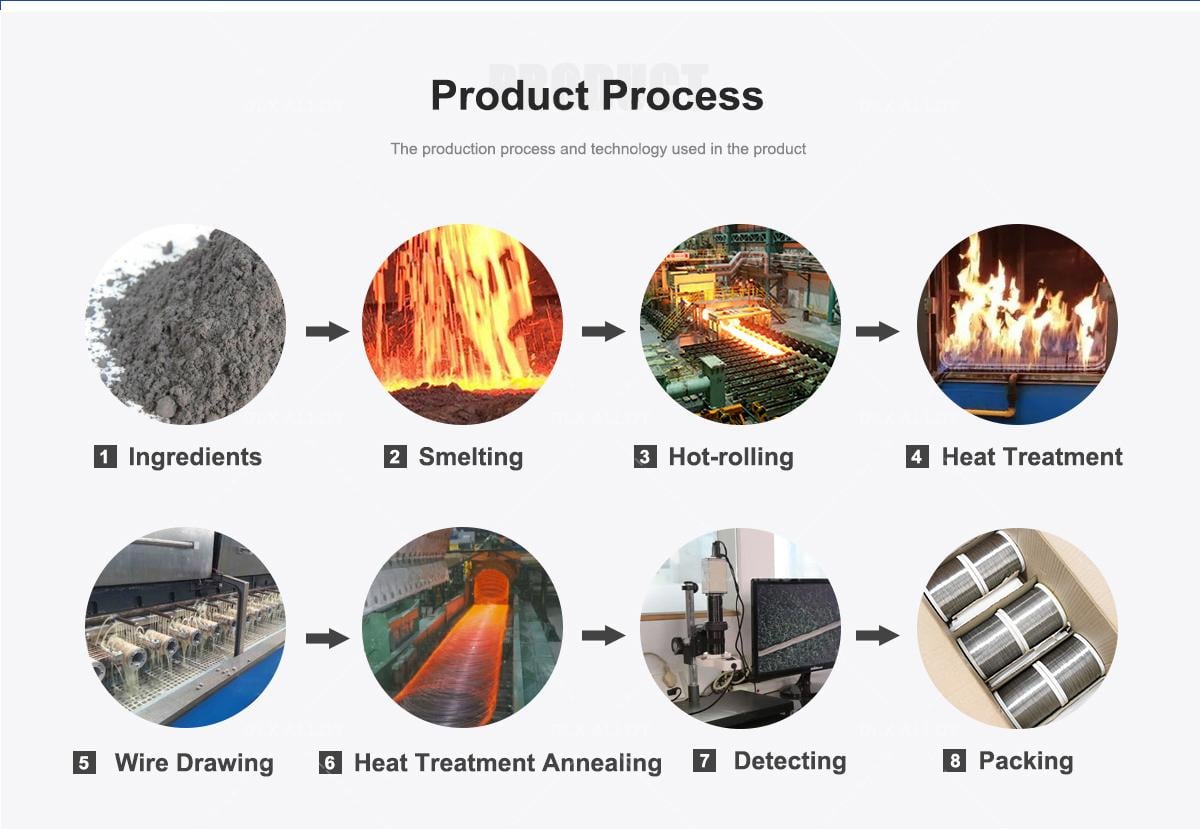
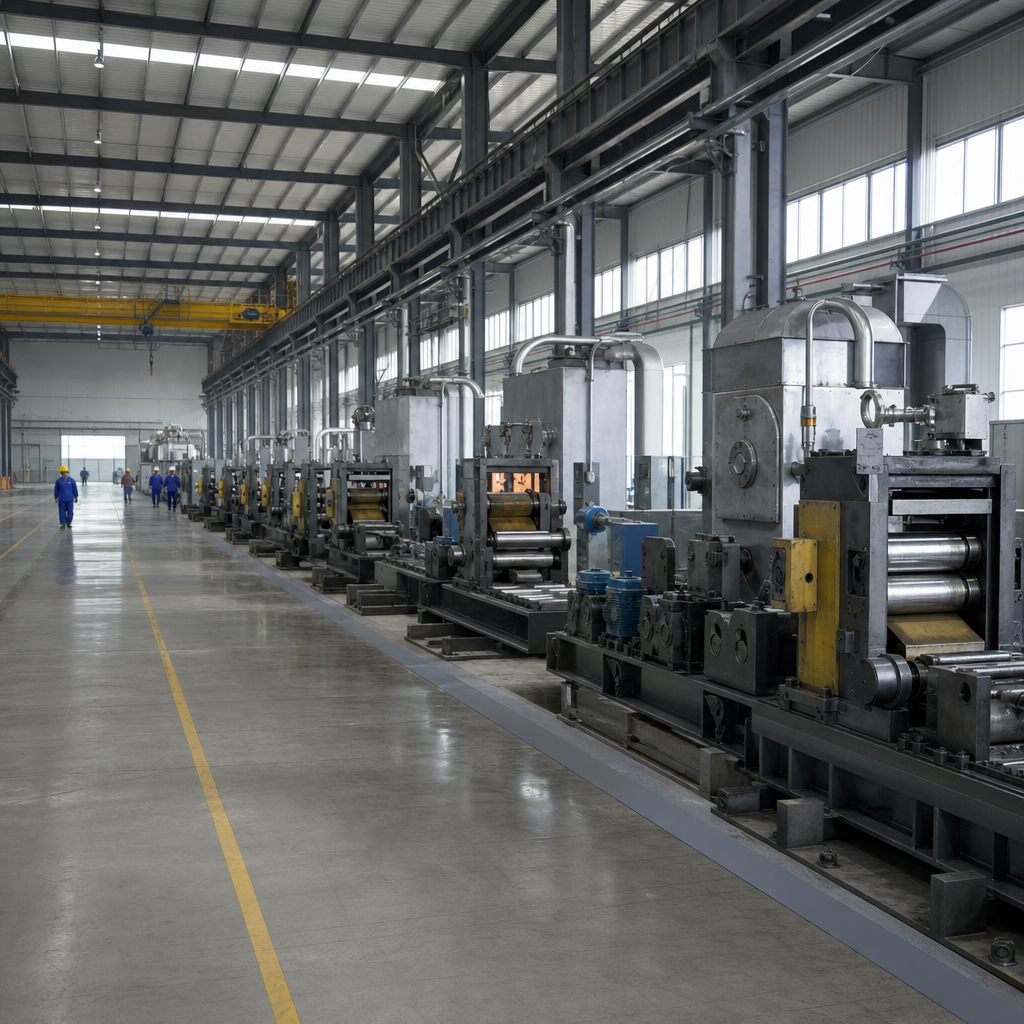
Integrated Production Chain: Complete in-house manufacturing from vacuum melting, hot rolling, wire annealing, precision cold drawing to final inspection.
-
Substantial Monthly Output: Robust production capacity reaching 1,200 tons/month, ensuring on-time delivery for bulk OEM and continuous manufacturing contracts.
-
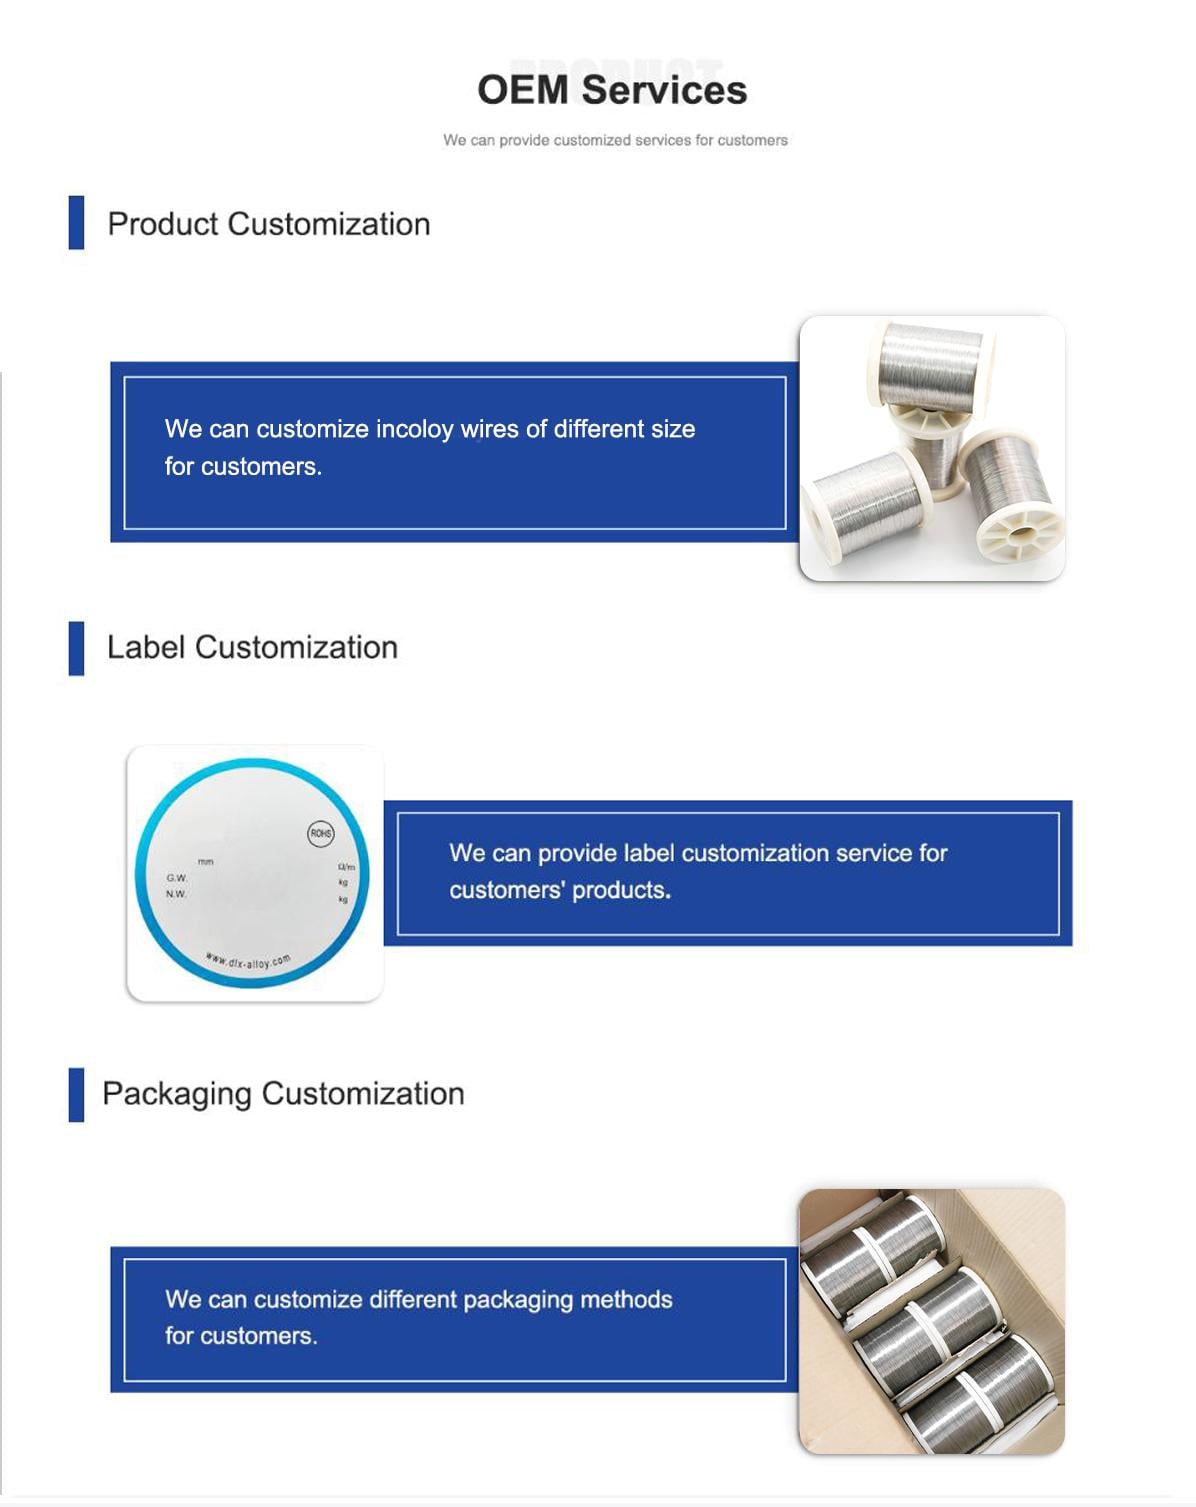
Custom Supply & Packaging Options:
-
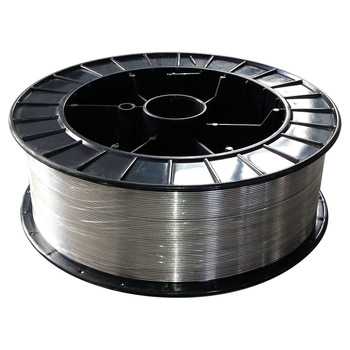
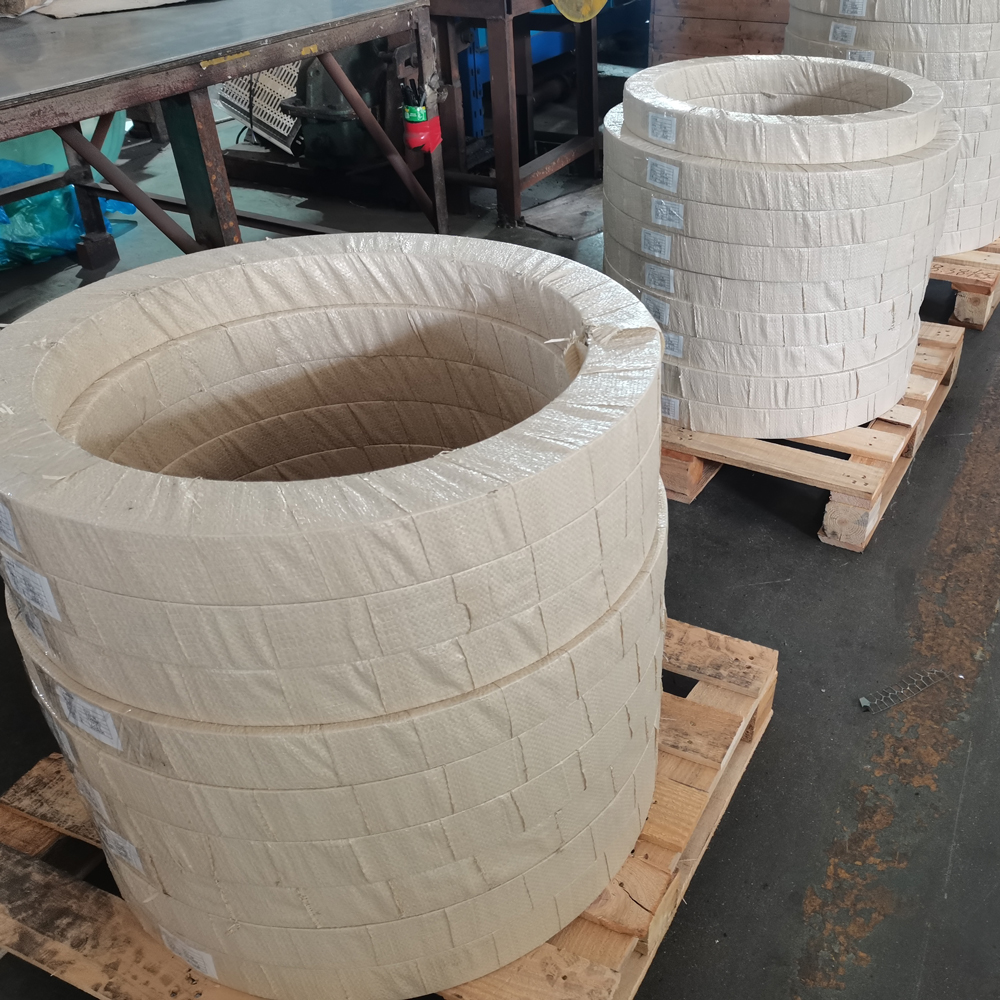
Spool / Carrier Coils: Available in continuous lengths (25 kg to 500 kg coils) with heavy-duty steel core carriers, waterproof wrapping, and custom palletizing to fit high-speed uncoilers.
-
Flexible Sizing: Tailored intermediate diameters and specific tensile windows tuned to your cold heading tooling requirements.
-
-
Direct Engineering Support: Full metallurgical traceability, mill test certificates (MTC) with actual chemical and mechanical values, and dedicated technical consultation for tool life optimization.
Frequently Asked Questions
Q1: What makes Incoloy 800HT preferable over standard Incoloy 800 for high-temperature fasteners?
A: Incoloy 800HT features a tightly controlled higher carbon window (0.06%–0.10%) combined with a mandatory titanium and aluminum addition (Al+Ti = 0.85%–1.20%) and a high-temperature solution anneal. This metallurgical balance provides substantially higher creep-rupture strength and structural stability at temperatures above 600°C (1112°F) compared to standard 800 series alloys.
Q2: Can this 0.8mm–5.0mm coil wire be processed directly in high-speed cold heading machines?
A: Yes. Our precision drawing process includes tailored intermediate bright annealing that delivers an optimal elongation rating (≥30%) and balanced hardness. This permits severe cold upset forming, collar forming, and thread rolling without pre-heating, extending die life and preventing head cracking.
Q3: How do you guarantee consistent diameter tolerances across an entire 200kg+ wire coil?
A: We employ dual-axis real-time laser gauging throughout the multi-pass cold drawing process. This maintains consistent diameter variation within ±0.015mm and out-of-round tolerances below 0.01mm, eliminating feeding jams in automatic CNC and multi-die fastener forming equipment.
Q4: What surface finishes are available for this fastener wire?
A: We supply wire with a clean Bright Annealed finish, pickled finish, or with light proprietary carrier coatings (copper-free / phosphate-free high-temperature drawing lubricants) designed to reduce friction and tooling wear during fastener cold forming.
Q5: What is the typical MOQ and packaging format for overseas shipment?
A: Minimum order quantities are flexibly configured based on target diameter specifications and production runs. Packaging options include precision-wound spools, catch-weight coils on metal formers, or wooden crates wrapped in multi-layer moisture-proof barrier films and steel strapping to ensure zero transit damage.