EN
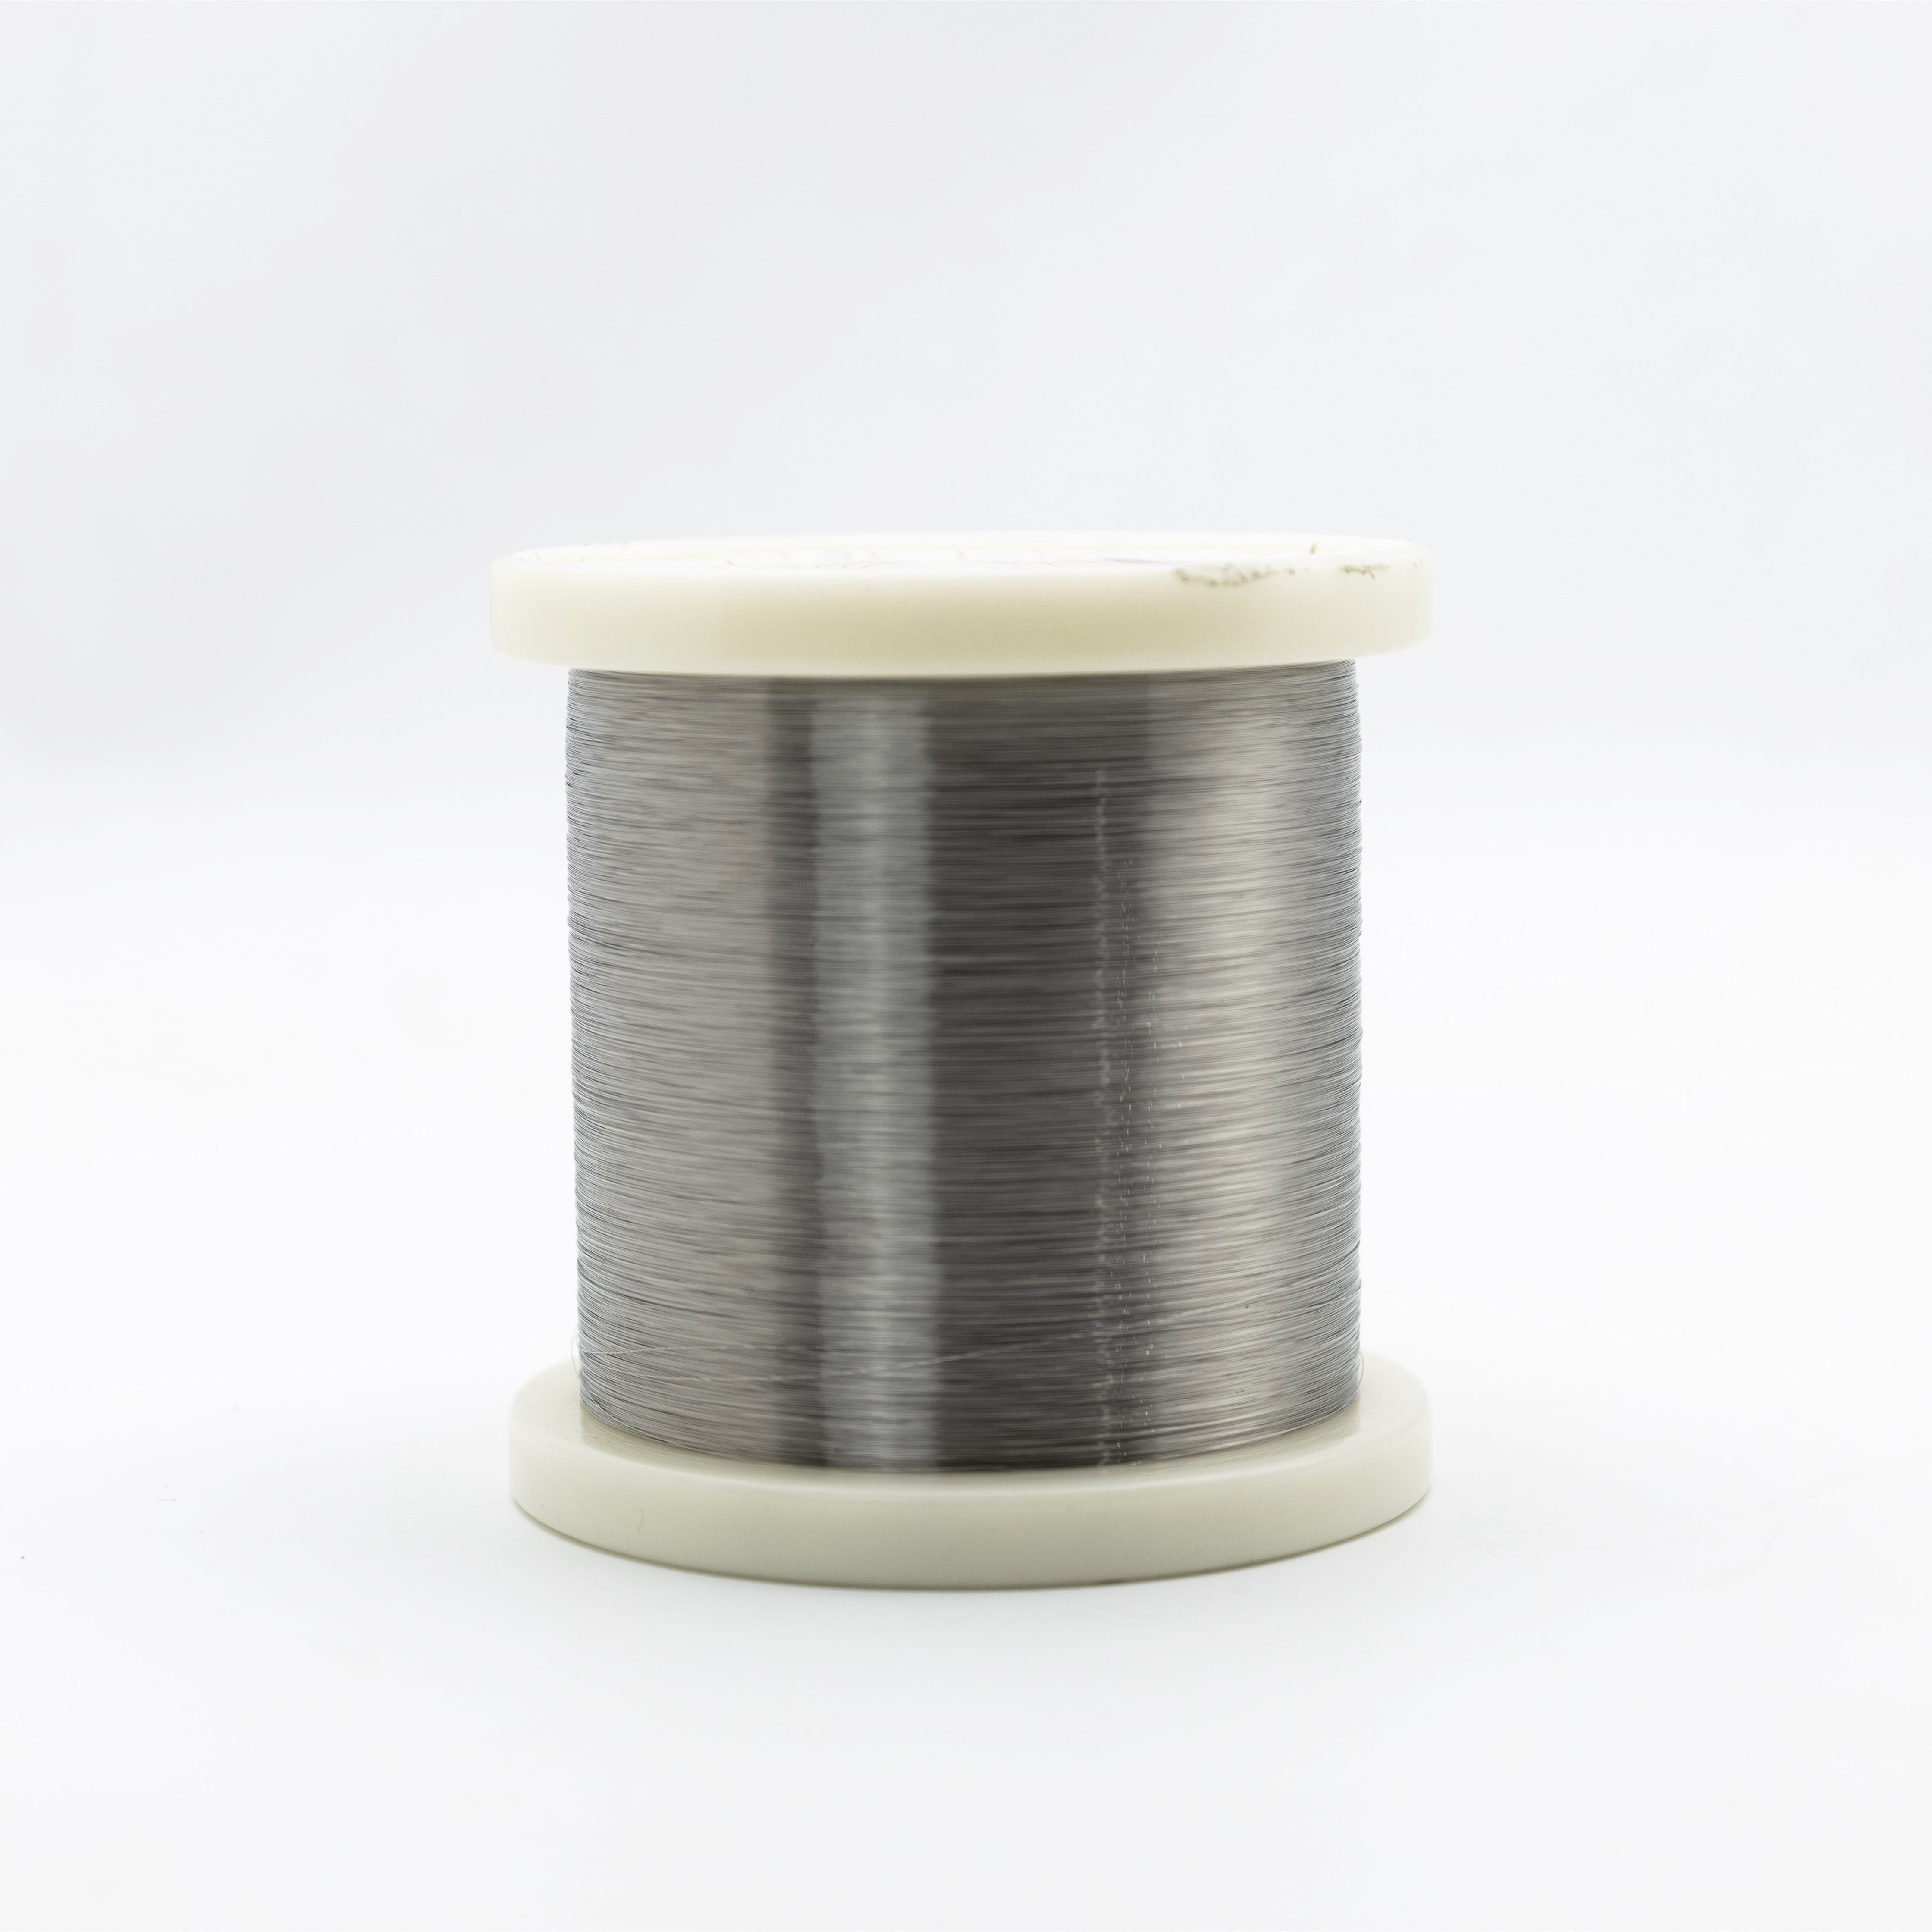
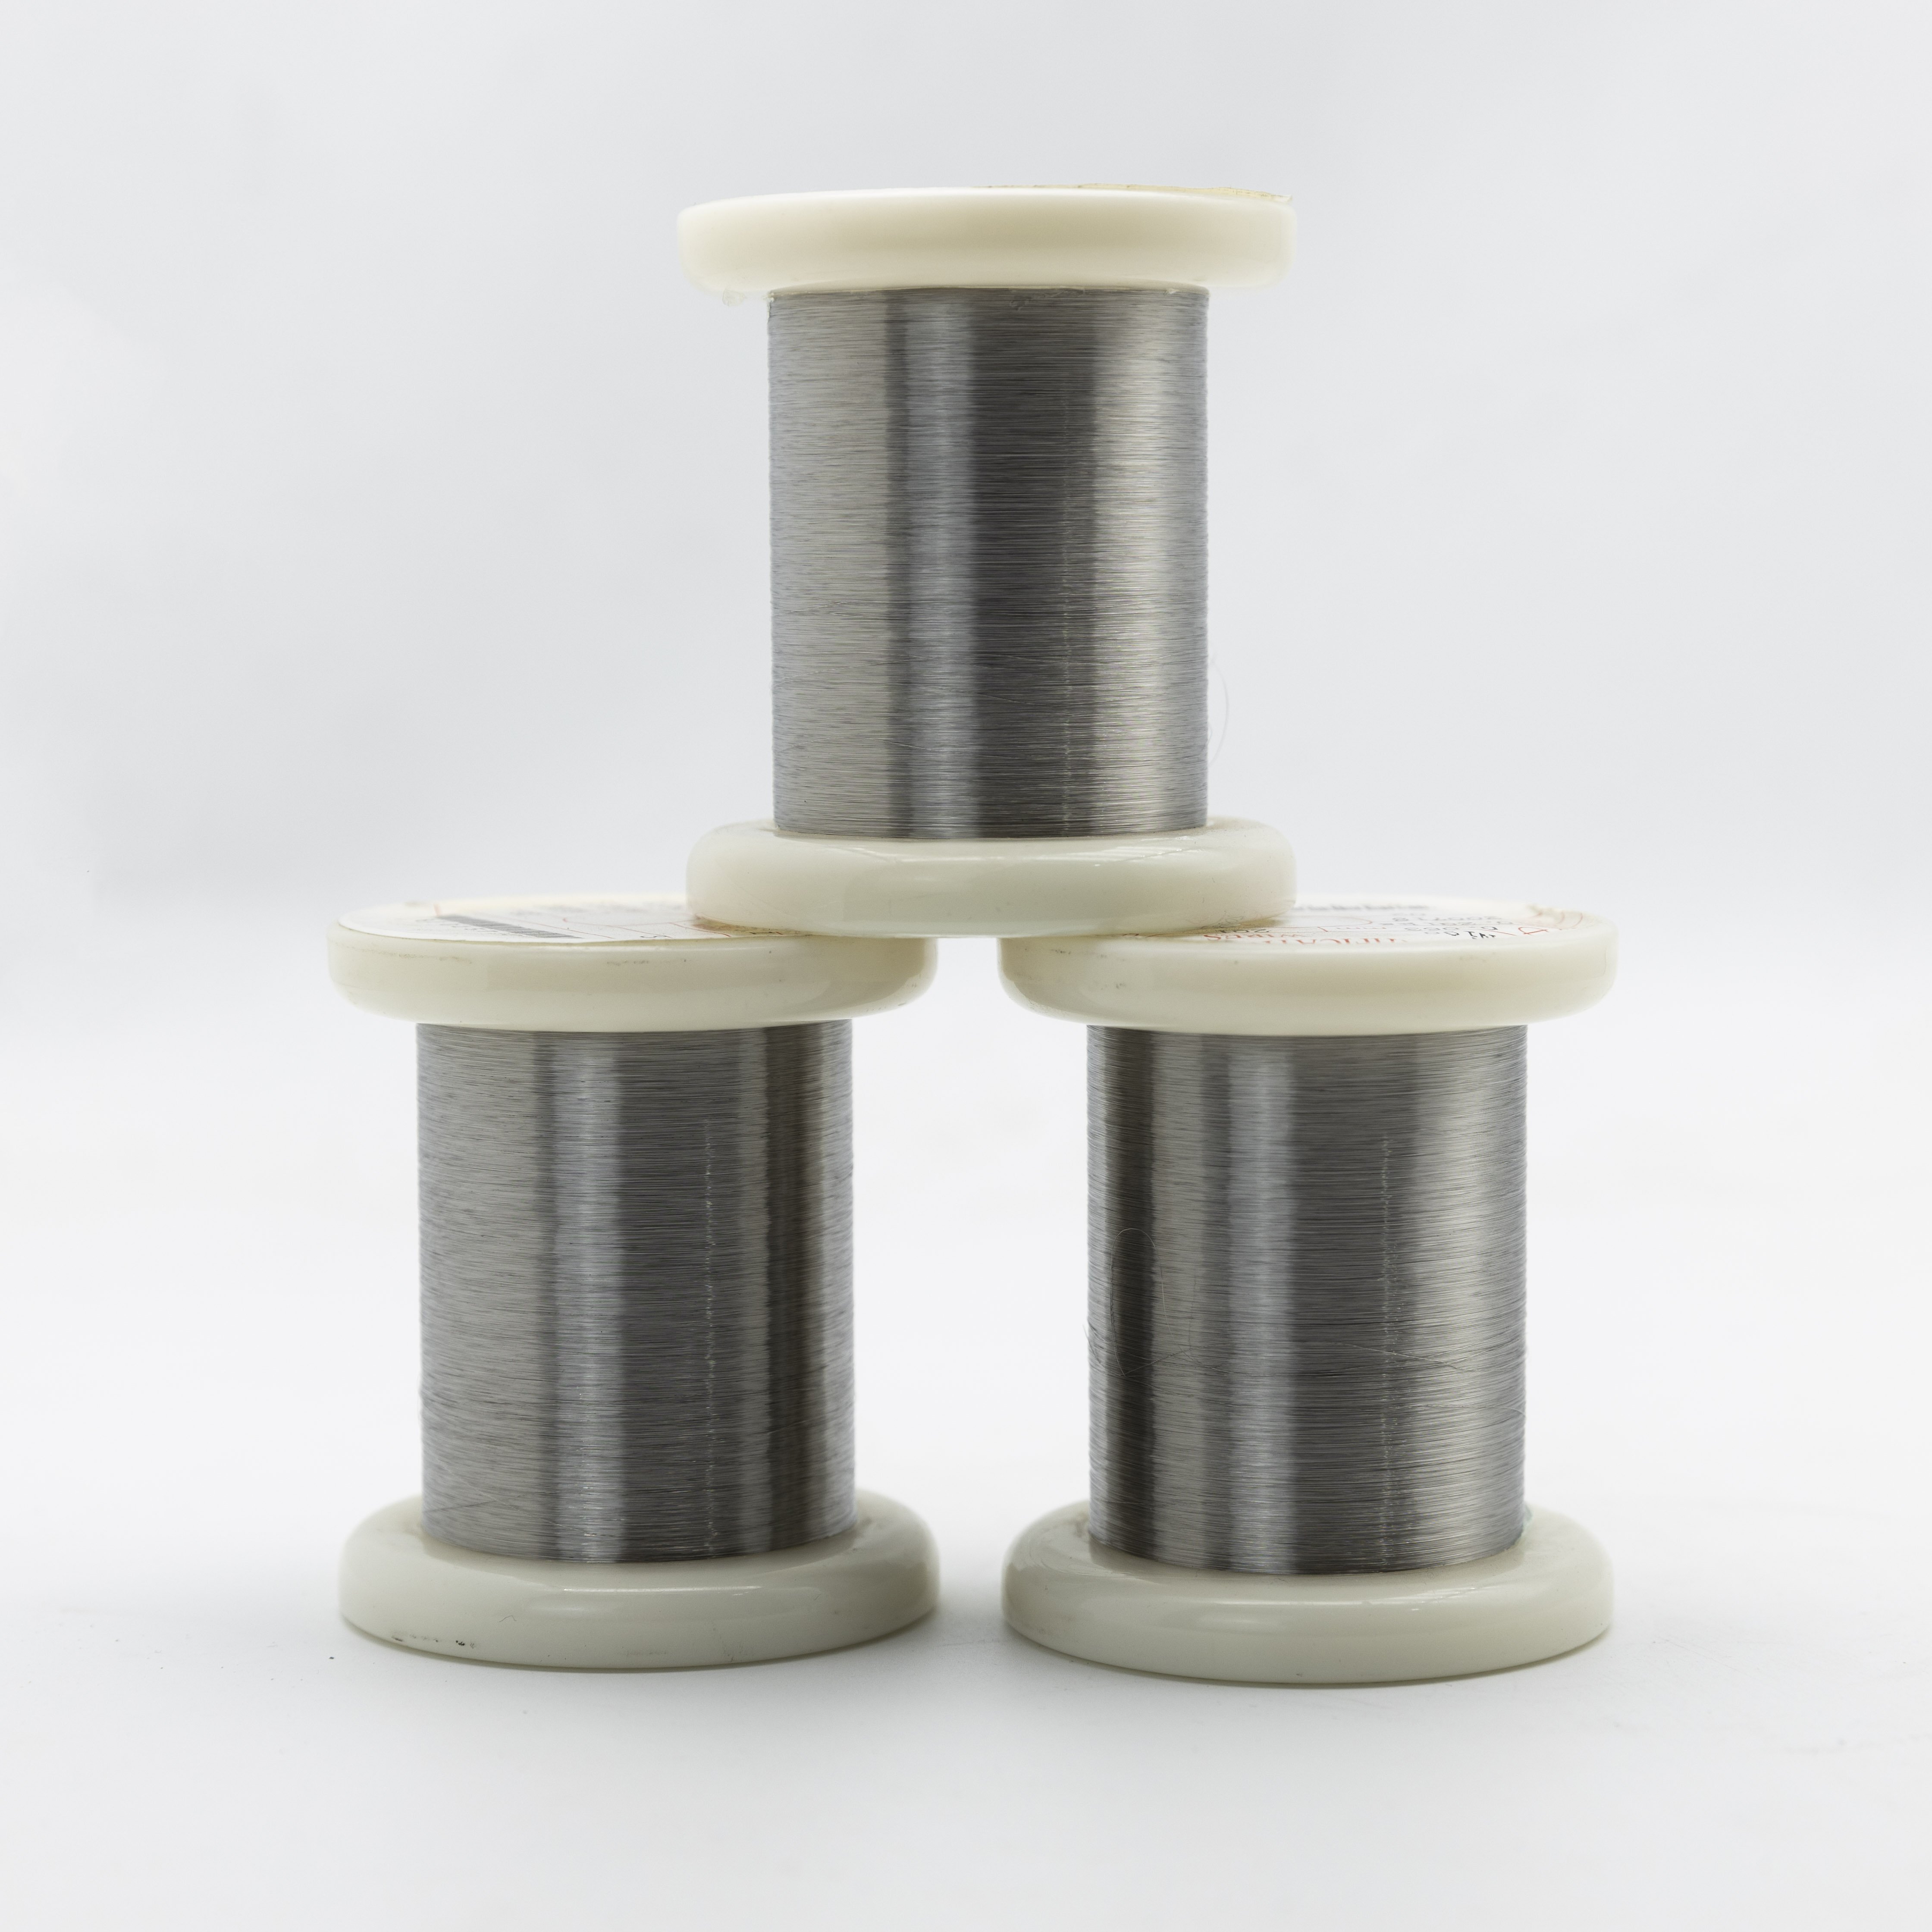
Premium Welding Wire Incoloy 800H Dia 1.2mm-4.0mm for Petrochemical Piping Fabrication
Engineered for severe thermal and corrosive refinery environments, our double-melted Incoloy 800H welding wire delivers ultra-stable arc characteristics, superior creep-rupture strength above 600°C, and micro-precision wire feeding across automated piping fabrication systems.
- Overview
- Key Features
- Specifications
- Applications
- Why-Us
- FAQ
- Recommended Products
Product Overview
High Temperature Incoloy 800H Welding Wire for Petrochemical Piping Fabrication
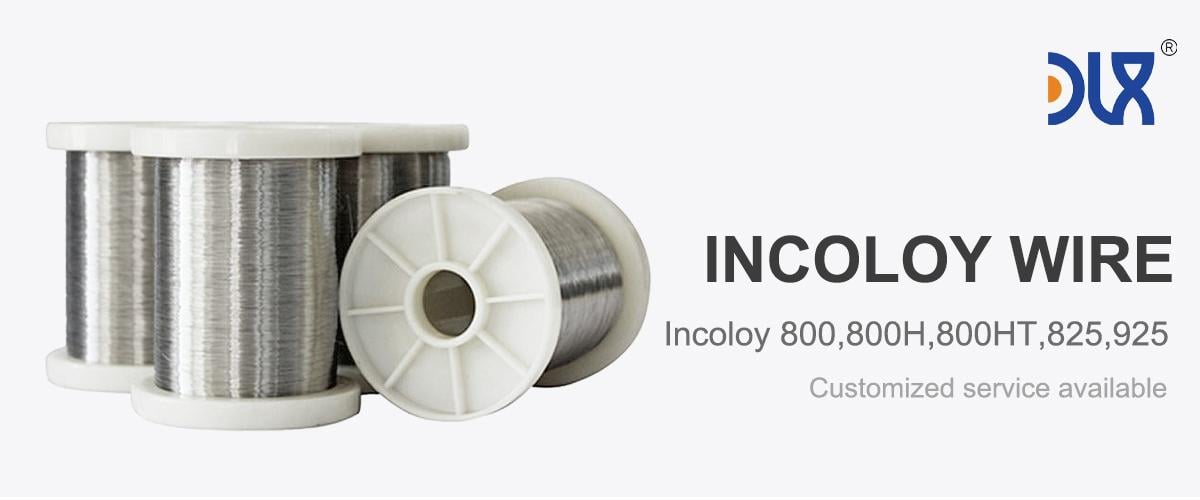
In high-stress thermal processing environments, weld joint reliability determines the overall safety and lifespan of critical infrastructure. Our Incoloy 800H welding wire is precisely formulated to match the thermal expansion and mechanical properties of alloy 800H/800HT base materials.
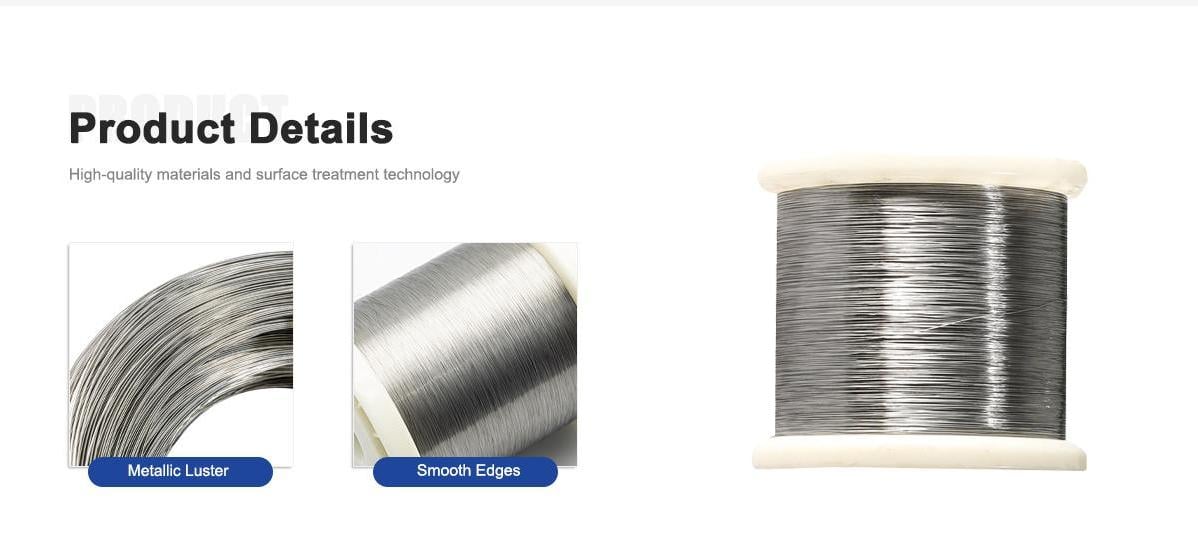
With optimized carbon, aluminum, and titanium ratios, this high temperature welding wire produces crack-free, micro-clean weld seams that withstand long-term thermal cycling and aggressive carburizing atmospheres in petrochemical piping fabrication, high-pressure steam headers, and ethylene cracking furnaces. Every spool and drum undergoes rigorous precision layer-winding and direct optical inspection to ensure smooth, uninterrupted feeding during automatic, semi-automatic, and manual welding operations.
Key Features
Precision Incoloy 800H Welding Wire Mechanical & Thermal Properties
-
Superior High-Temperature Creep-Rupture Strength: Carefully controlled carbon chemistry delivers sustained structural integrity and high creep resistance under prolonged exposure to temperatures up to 1000°C (1832°F).
-
Outstanding Resistance to Carburization & Oxidation: Dense, self-healing oxide films prevent carbon ingress and high-temperature scaling in cyclic petrochemical environments.
-
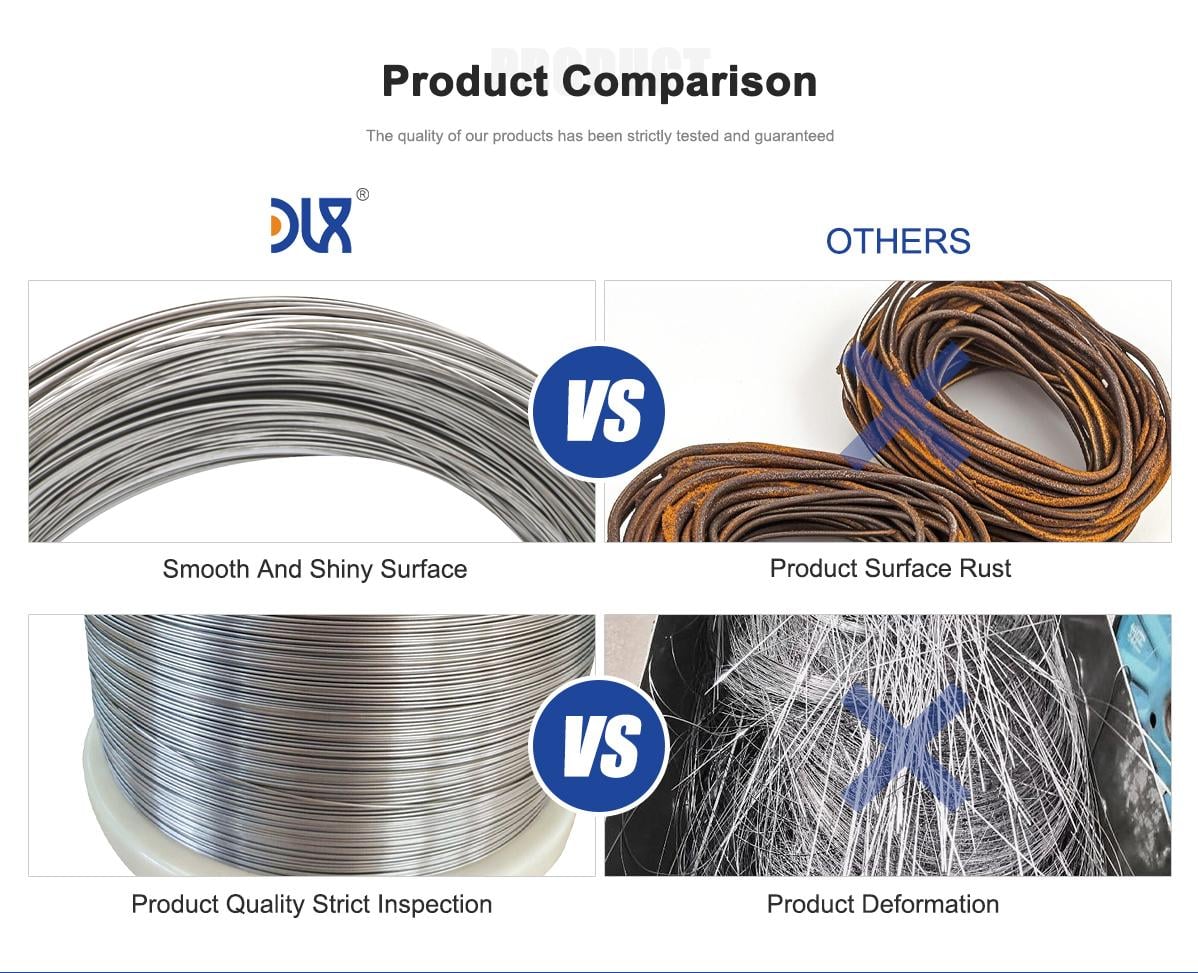
Flawless Wire Feedability & Precision Tolerances: Manufactured with micro-level diameter tolerance (±0.01mm) and smooth surface finishing, eliminating feed jams in automated GMAW/GTAW systems.
-
Ultra-Clean Metallurgical Quality: Produced via double-melt refining to minimize harmful non-metallic inclusions, gases, and trace impurities, preventing hot cracking and porosity during root and fill passes.
-
Uniform Chemical Composition & Microstructure: Guaranteed lot-to-lot consistency ensures reproducible weld pool fluidity, stable arc characteristics, and minimal post-weld cleanup.
Technical Specifications & Dimension Range
| Parameter | Specification & Engineering Data |
|---|---|
| Product Form | Precision Spooled Wire (MIG/GMAW), Straight Rods (TIG/GTAW) |
| Diameter Range | 1.2mm, 1.6mm, 2.0mm, 2.4mm, 3.2mm, 4.0mm (Custom gauges available) |
| Diameter Tolerance | ±0.01mm for high-speed automated feeding stability |
| Material Base | Nickel-Iron-Chromium High-Temperature Solid Solution Alloy |
| Primary Process | VIM (Vacuum Induction Melting) + ESR (Electroslag Remelting) + Cold Drawing |
| Surface Finish | Bright, smooth, de-greased, free from scuffs, slivers, or lubricants |
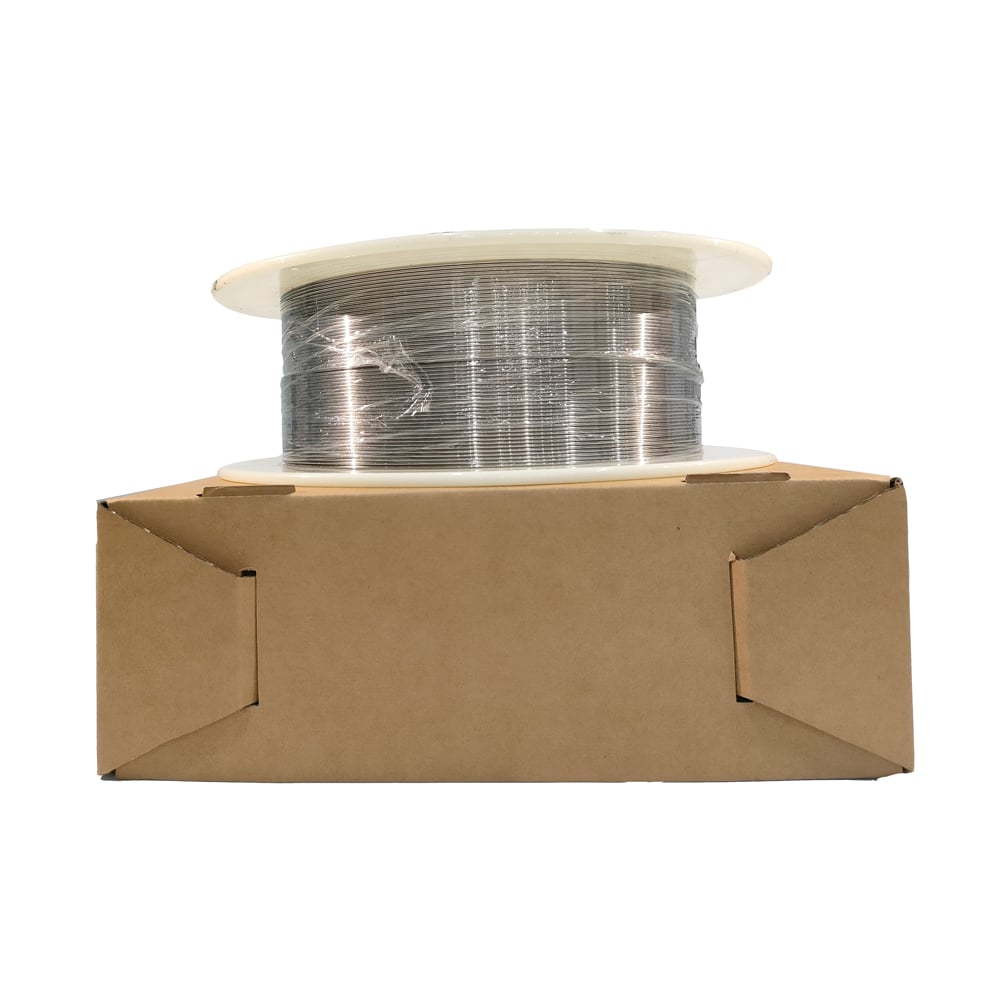
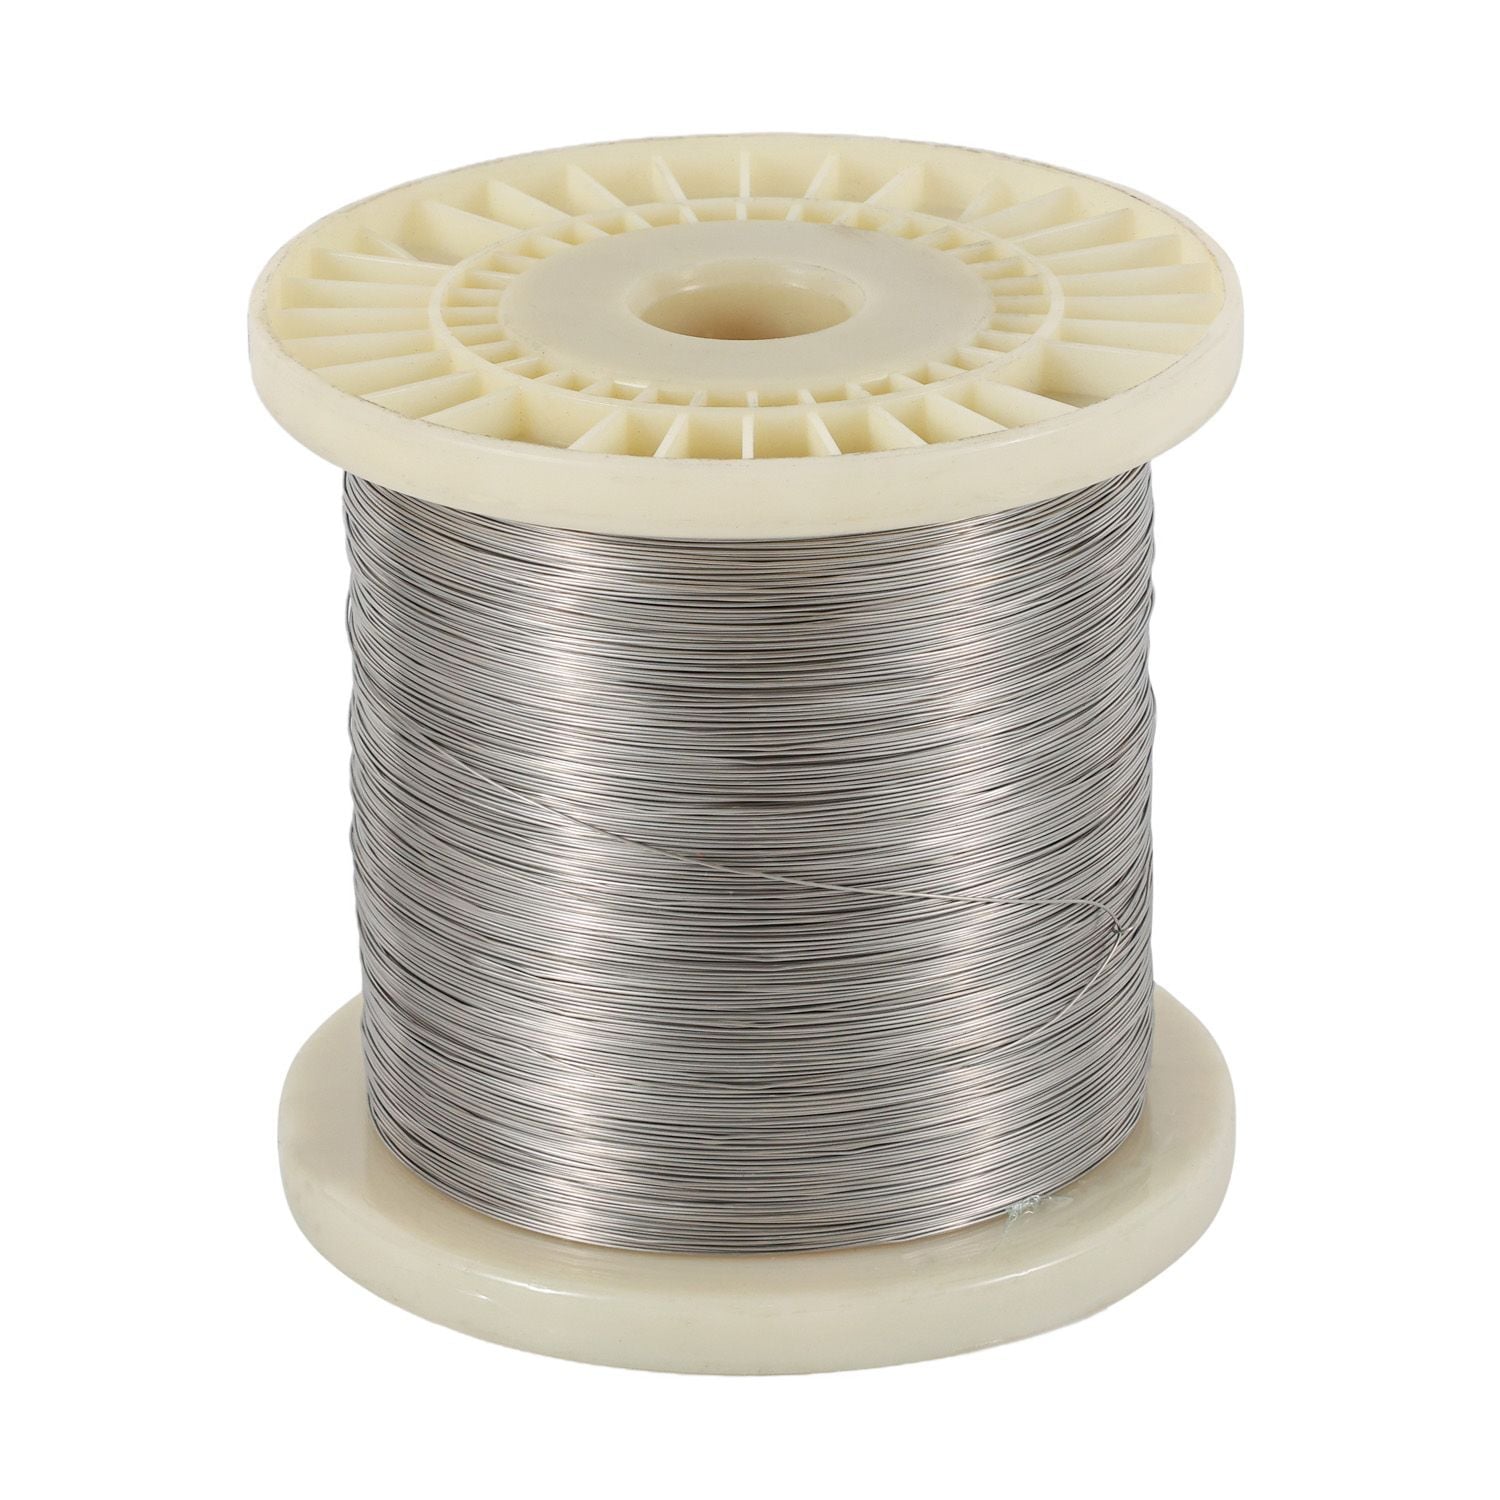
| Standard Packaging | 12.5kg / 15kg Precision Layer Spools (MIG) |
Industrial Applications
Petrochemical Piping Fabrication & Thermal Equipment
-
Petrochemical & Refining Piping Fabrication: Ideal for joining and overlaying transfer lines, reforming tube connections, steam methane reformer pigtails, and cracking furnace manifolds.
-
Industrial Furnace & Heat Treating Components: Critical fabrication of radiant tubes, muffle retorts, furnace baskets, and high-temperature heat exchangers.
-
Power Generation & Nuclear Systems: Welding of high-temperature superheater piping, steam re-heaters, and high-pressure vessel nozzles.
-
Chemical Processing Reactors: Fabrication of nitric acid and organic chemical equipment requiring simultaneous corrosion and thermal resistance.
Why Partner with DLX
Leading High-Temperature Nickel Alloy Manufacturing Capability
-
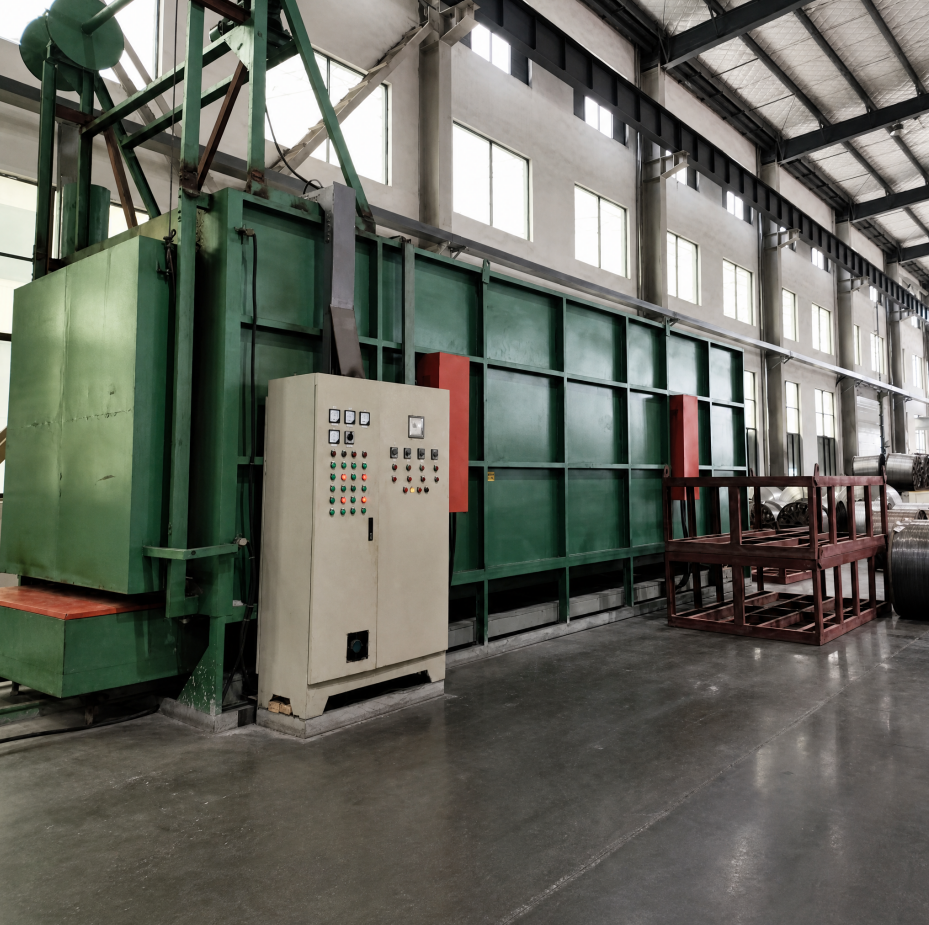
Dedicated Scale & Massive Monthly Capacity: Operating a modern, integrated metallurgical facility with an established monthly production capacity of 1,200 metric tons, ensuring dependable lead times for large-scale engineering contracts.
-
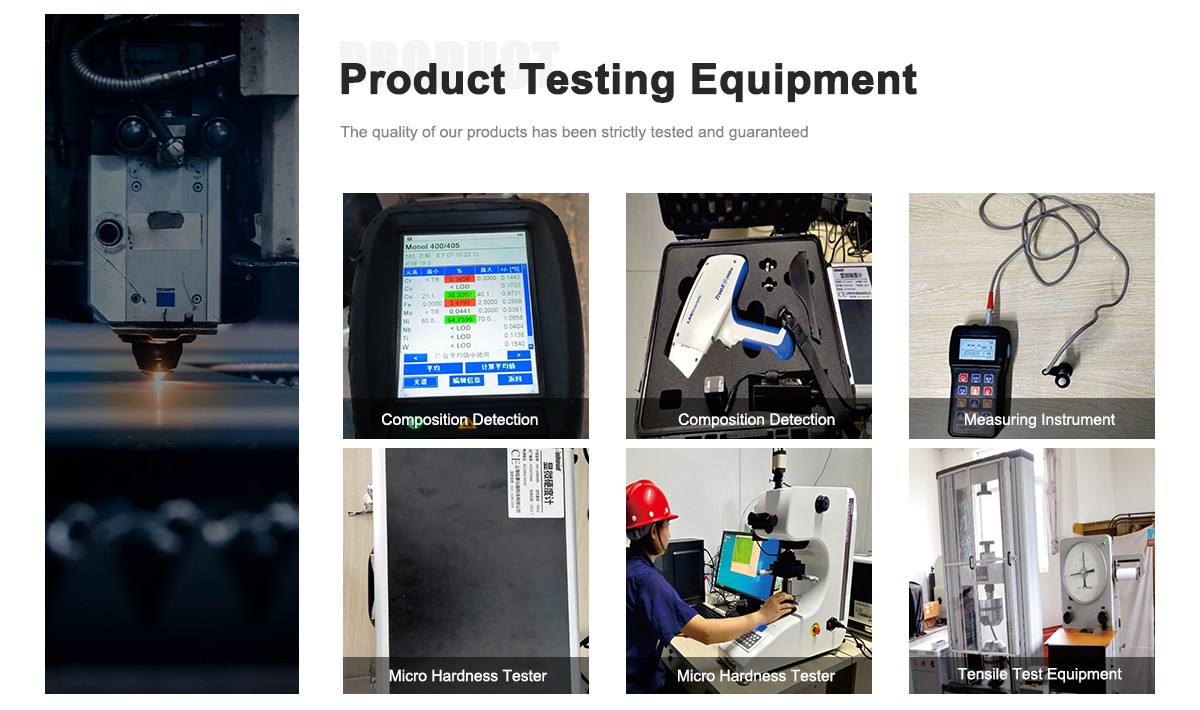
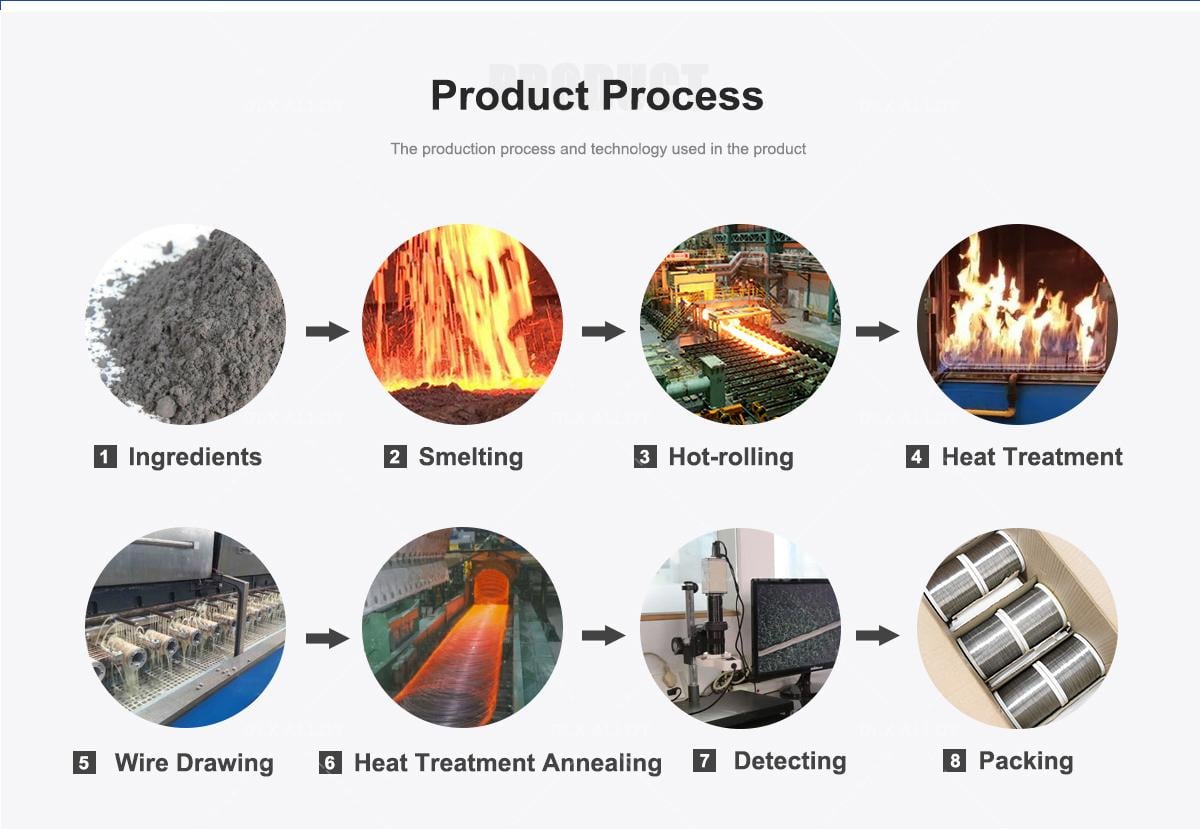
Full Traceability & In-House Testing: Complete 100% batch testing—including PMI chemical verification, eddy current surface testing, and dimensional profiling—delivering comprehensive mill test reports for critical energy projects.
-
Engineered for High-Efficiency Welding: Precision layer-wound spools and micro-polished surfaces reduce contact tip wear and enhance robotic welding productivity.
-
Flexible Industrial Procurement: Dynamic MOQ options based on spool/drum configurations and custom alloy sizing, tailored specifically for EPC contractors, piping fabricators, and OEM manufacturers.
Frequently Asked Questions
Q1: What welding processes are suitable for this 1.2mm–4.0mm Incoloy 800H wire?
A1: Our wire is fully optimized for Gas Tungsten Arc Welding (GTAW/TIG), Gas Metal Arc Welding (GMAW/MIG), and Submerged Arc Welding (SAW). Smaller diameters (1.2mm–1.6mm) are layer-wound for MIG and automatic orbital welding, while larger sizes (2.0mm–4.0mm) are available as straight cut lengths for TIG or heavy spool drums for automated line fabrication.
Q2: How does Incoloy 800H welding wire prevent hot cracking in high-temperature petrochemical piping?
A2: Hot cracking is mitigated through strict raw material selection and ultra-clean double-vacuum melting processes. By strictly controlling trace tramp elements (such as sulfur and phosphorus) and balancing ferrite-promoting/stabilizing micro-elements, our wire provides a stable, crack-resistant solidification structure.
Q3: What shielding gas mixture is recommended for MIG/TIG welding with this filler wire?
A3: For TIG welding, 100% high-purity Argon is recommended. For MIG welding of petrochemical piping, an Argon-Helium blend or Argon with small additions of reducing gases (e.g., 98% Ar + 2% CO2 or Ar/He mixtures) ensures optimal arc stability, smooth wetting action, and deep root penetration.
Q4: Can DLX provide customized spool weights and packaging for automated fabrication lines?
A4: Yes. We supply precision layer-wound 12.5kg/15kg spools, 100kg–250kg bulk payoff drums for continuous robotic welding cells, and rigid waterproof boxed straight lengths with embossed identification on each rod.