EN
High-Temp Incoloy 800H Precision Strip 0.2-2.5mm for Expansion Joint Bellows
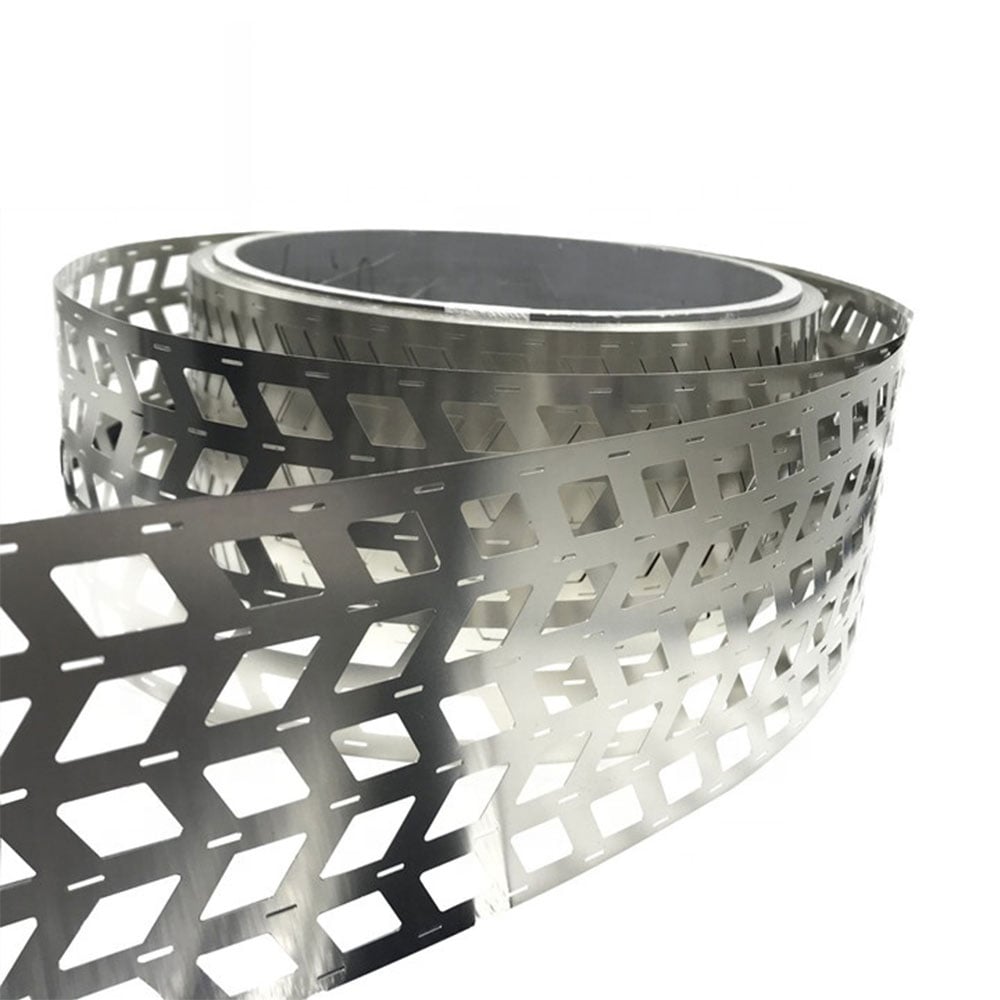
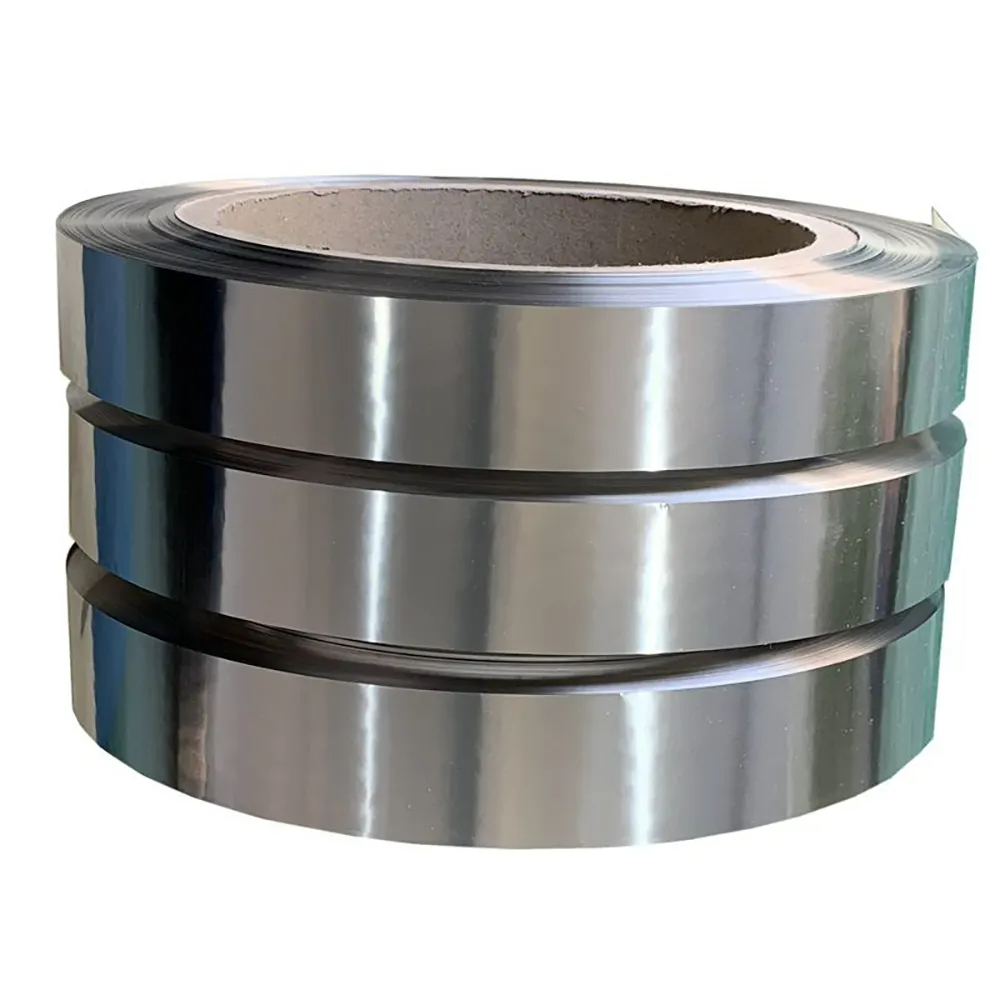
Premium solution annealed Incoloy 800H precision strip (thickness 0.2mm to 2.5mm) custom-manufactured for multi-ply and single-ply expansion joint bellows. Featuring tightly controlled grain sizing, ultra-low residual stress, and exceptional creep rupture resistance at temperatures up to 980°C.
- Overview
- Key Features
- Specifications
- Applications
- Why-Us
- FAQ
- Recommended Products
Product Overview
Metallurgy & Performance of Incoloy 800H Precision Strip
Incoloy 800H is an advanced austenitic solid-solution alloy fortified with precisely balanced carbon (0.05% - 0.10%) and combined aluminum plus titanium additions (0.85% - 1.20%). When processed into thin-gauge precision strip (0.2mm - 2.5mm) and subjected to our high-temperature solution annealing cycle, the alloy develops an optimal, uniform coarse austenitic grain structure (typically grain size 5 or coarser).
This controlled microstructure maximizes long-term creep-rupture strength at sustained operating temperatures above 600°C (1112°F) and up to 980°C (1796°F). Designed to handle cyclic thermal expansion, mechanical vibration, and axial/lateral angular deflection, our strip ensures structural integrity in petrochemical pipelines, thermal power exhausts, and aerospace ducting systems without micro-cracking during hydroforming or mechanical roll-forming.
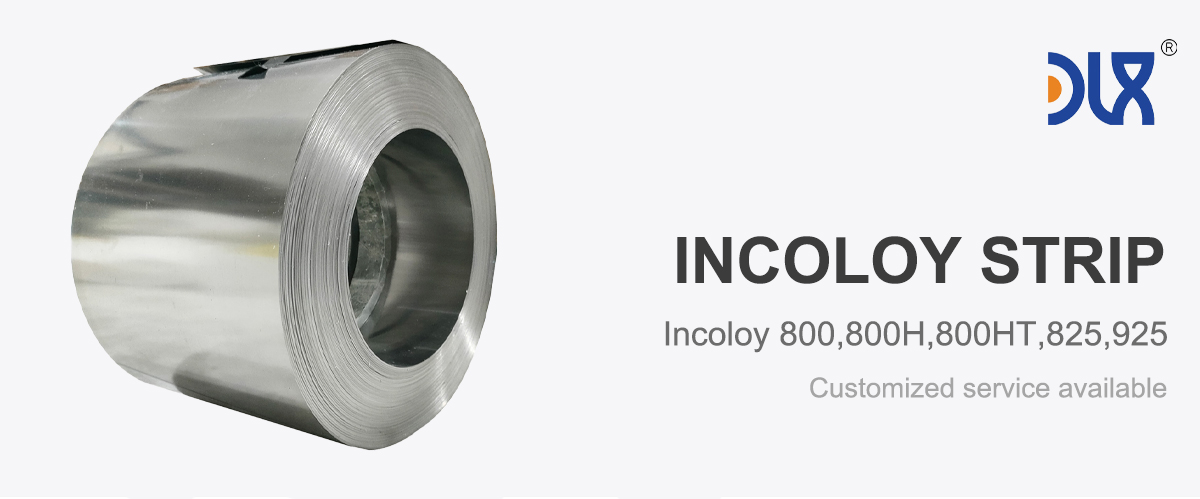
Key Features of Solution Annealed Incoloy 800H Strip (0.2mm-2.5mm)
-
Superior High-Temperature Creep Rupture Strength: Formulated with optimized titanium-aluminum-carbon ratios to maintain structural rigidity and resist metallurgical sag under continuous high thermal and mechanical stress.
-
Ultra-Fine Dimensional & Thickness Tolerances: Precision-rolled on advanced 20-high Sendzimir rolling mills, achieving thickness uniformity within +/-0.005mm to ensure consistent wall thickness across complex bellows convolutions.
-
Controlled Grain Sizing for Extended Cycle Fatigue Life: Solution annealing parameters are precisely monitored to balance grain coarseness for creep resistance with surface ductility for multi-cycle fatigue endurance.
-
Exceptional Deep-Drawing & Forming Ductility: High elongation (≥35%) and burr-free, custom-deburred slit edges ensure flawless performance in continuous roll-forming, elastomer bulging, and high-pressure hydraulic forming.
-
High Oxidation & Carburization Resistance: Stable chromium-nickel protective oxide scale prevents surface degradation in sulfur-bearing, carburizing, and high-temperature flue gas environments.
-
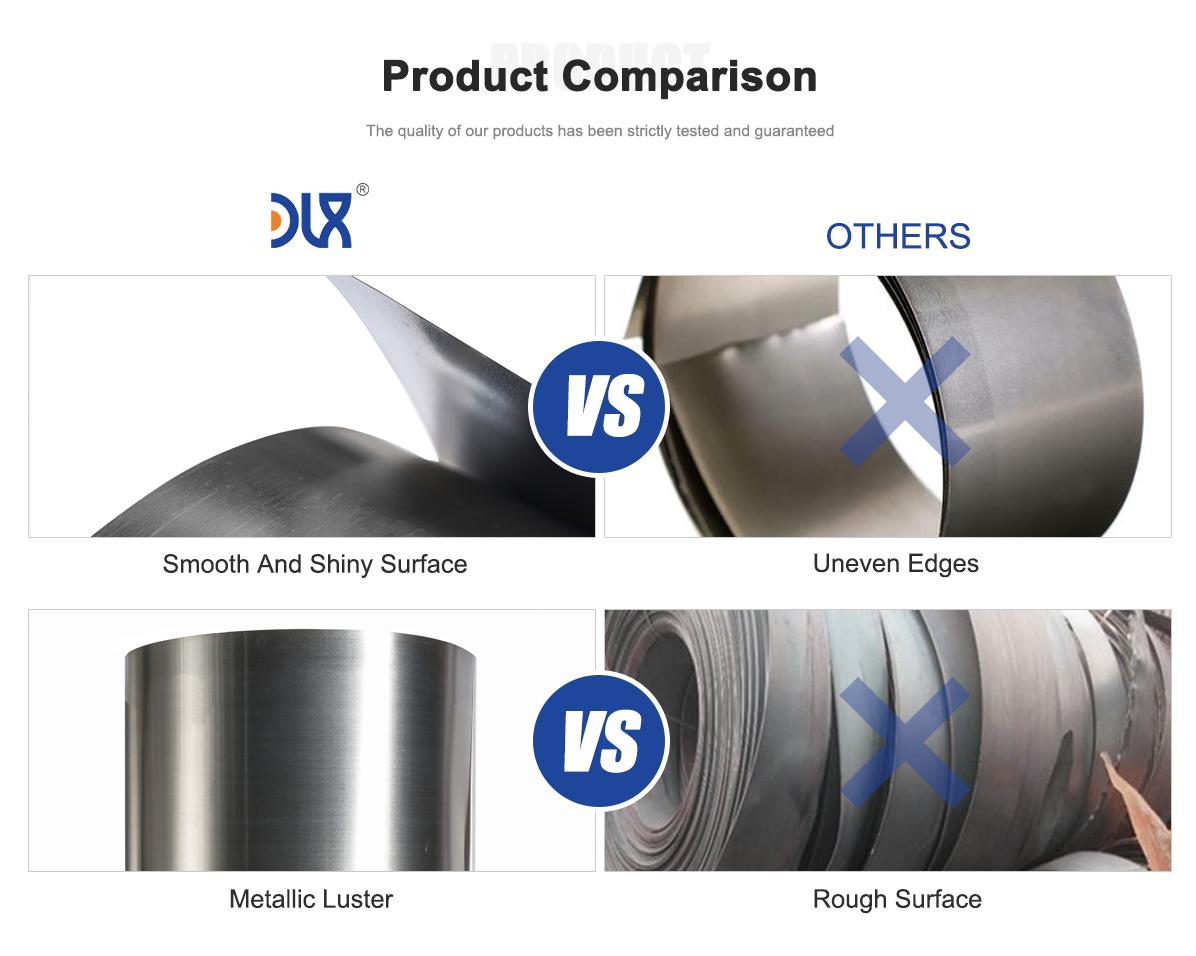
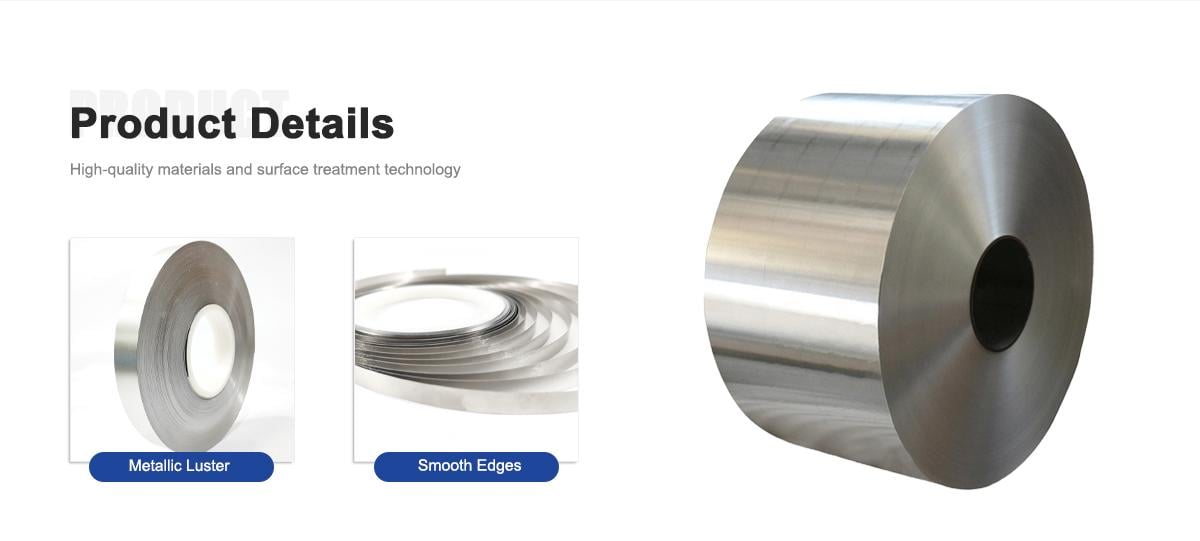
Pristine Bright Annealed Surface: Ra ≤ 0.2µm bright-annealed finish free from scale, oil residues, scratches, and pinholes, eliminating localized stress concentration zones.
High-Performance Technical Specifications for Bellows Fabrication
| Parameter / Item | Specification & Manufacturing Capability |
|---|---|
| Material Grade | Incoloy 800H |
| Thickness Range | 0.20 mm – 2.50 mm (Custom ultra-fine gauges available upon request) |
| Width Range | 10 mm – 650 mm (Precision slit coils or cut-to-length flat sheets) |
| Delivery Condition | Solution Annealed |
| Surface Finish | 2B / BA (Bright Annealed, Ra ≤ 0.2 µm) |
| Edge Conditions | Precision slit edge, deburred edge, rounded safety edge |
| Grain Structure Control | Controlled uniform grain size distribution for high-temperature creep & fatigue resistance |
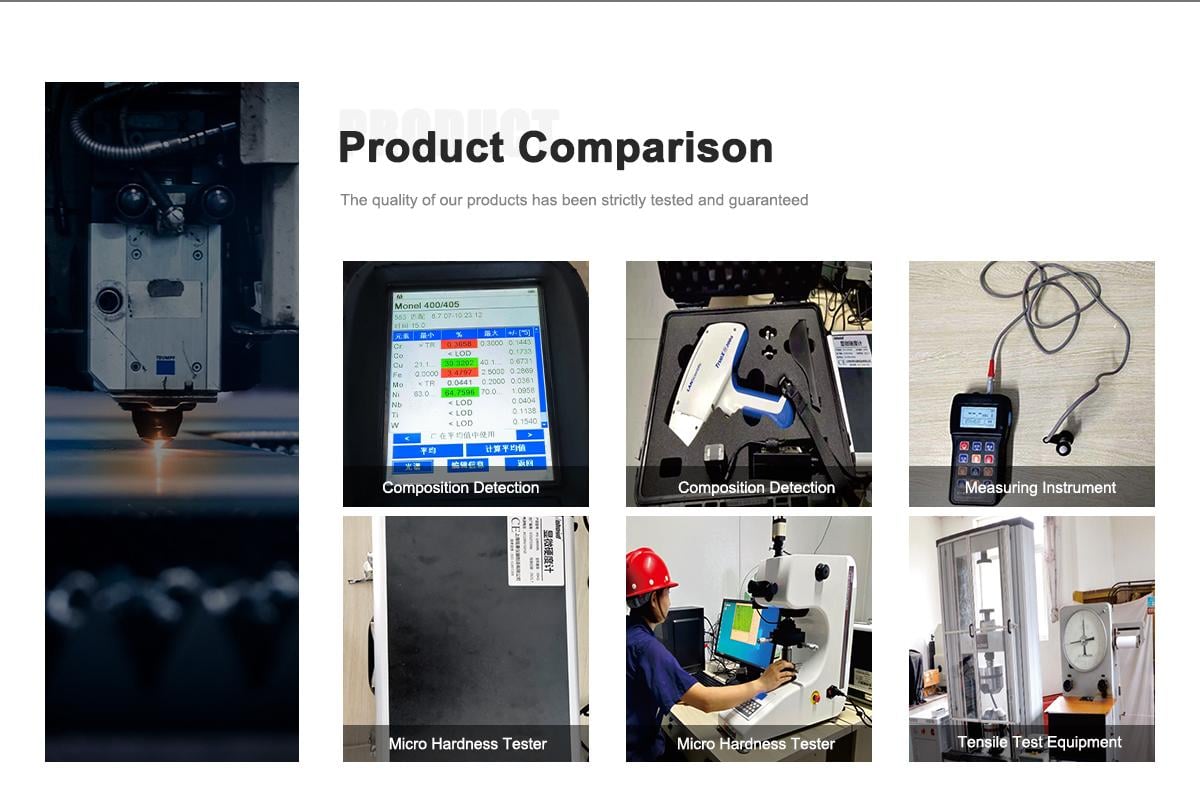
| Quality Verification | 100% Eddy Current testing, optical microstructural analysis, tensile verification, and laser thickness gauging |
Industrial Applications for Incoloy 800H Expansion Joint Bellows Strip
-
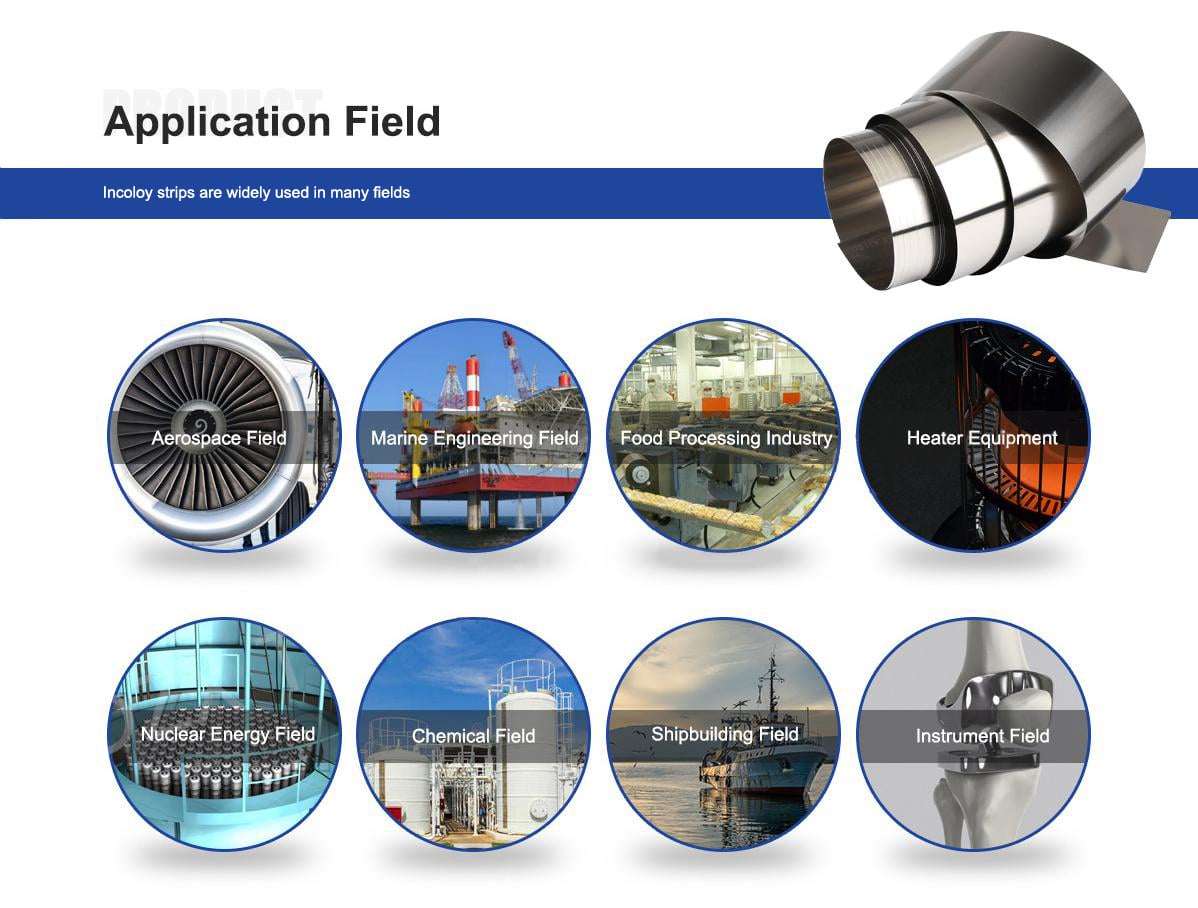
Exhaust & Ducting Expansion Joints: Multi-ply and single-ply flexible bellows for gas turbine exhaust systems, diesel engine manifolds, and thermal power plant piping.
-
Petrochemical & Refining Bellows: Catalyst regeneration piping, FCCU expansion joints, ethylene cracking furnaces, and high-temperature hydrocarbon transfer lines.
-
Nuclear & Power Generation: Steam generator flexible connections, boiler penetration seals, and heat recovery steam generator (HRSG) expansion units.
-
Industrial Furnace & Kiln Connections: High-temperature flue gas compensators, flexible duct connections, and radiant tube bellows.
-
Aerospace & Marine Ducting: High-pressure hot air duct expansion compensators and marine propulsion exhaust joints.
Why Choose DLX for High Temperature Solution Annealed Nickel Alloys
-
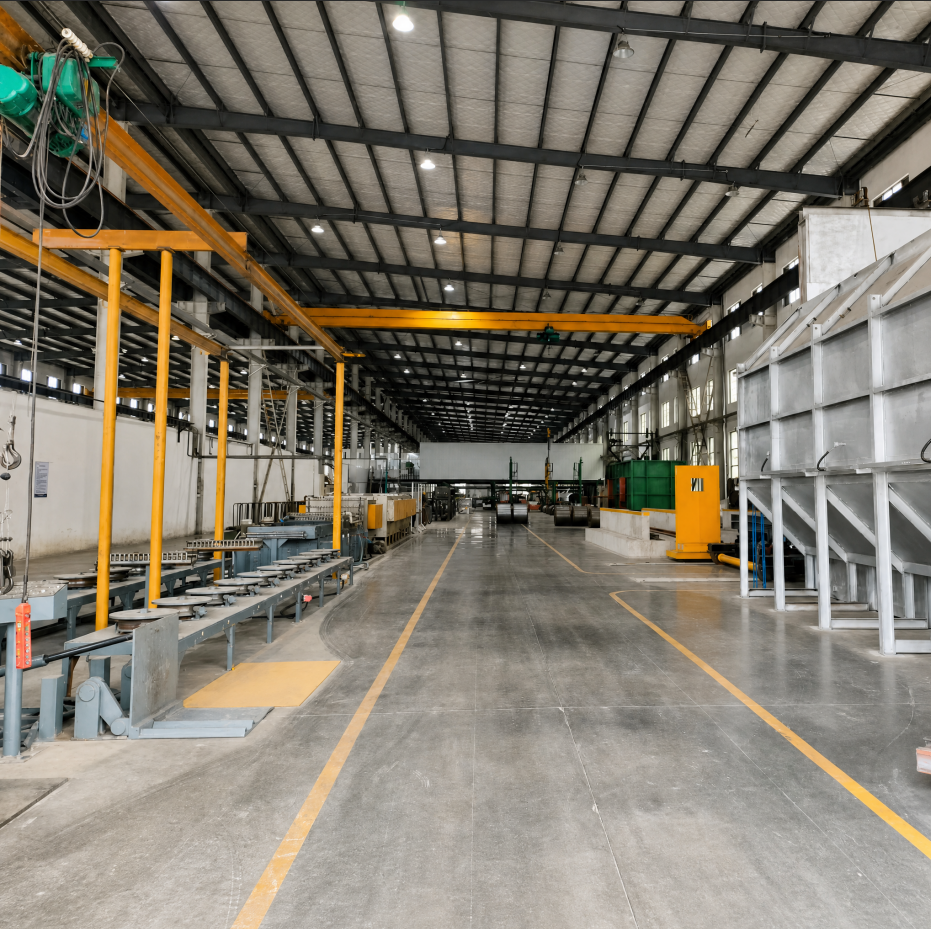
Integrated High-Purity Metallurgy: Complete internal production chain from VIM/ESR smelting, hot forging, and cold precision rolling to computerized continuous bright annealing furnaces.
-
Stringent Metallurgical & Grain Control: Proprietary thermal processing ensures zero incomplete recrystallization zones and strict batch-to-batch microstructural consistency.
-
Robust Manufacturing Capacity: With a stable monthly production capacity of 1,200 tons, DLX guarantees reliable volume delivery for major global expansion joint OEMs and engineering contractors.
-
Custom Slitting & Edge Engineering: In-house high-precision slitting lines provide tight width tolerances (+/-0.05mm), camber-free strip, and customized deburred edges to protect forming dies.
-
Full Traceability & Compliance: Every batch is delivered with full chemical analysis, mechanical property certificates, grain size verification reports, and non-destructive testing documentation.
Frequently Asked Questions About Incoloy 800H Bellows Strip
Q1: Why is Incoloy 800H preferred over standard Incoloy 800 for expansion joint bellows?
A1: Incoloy 800H contains a higher carbon range (0.05-0.10%) and is subjected to a specialized high-temperature solution annealing process that establishes a controlled coarse grain structure. This metallurgical design provides significantly higher creep and stress rupture strength at temperatures above 600°C compared to grade 800.
Q2: What thickness tolerances can DLX maintain on 0.2mm to 2.5mm Incoloy 800H strip?
A2: Using precision multi-roll Sendzimir cold rolling mills equipped with automated laser thickness gauges, we maintain thickness tolerances within +/-0.005mm to +/-0.015mm depending on the exact gauge, ensuring uniform wall thickness throughout bellows expansion.
Q3: How does your solution annealing process prevent cracking during hydroforming?
A3: Our continuous hydrogen bright annealing line strictly controls heating curves and cooling speeds. This produces a homogeneous microstructure with low residual internal stress and high elongation (≥35%), preventing micro-fissuring and work-hardening failures during hydraulic or mechanical convolution forming.
Q4: What is the Minimum Order Quantity (MOQ) and lead time for custom-slit Incoloy 800H coil?
A4: We offer flexible MOQs adapted to specific strip gauges, slit widths, and manufacturing schedules (starting from trial batches for prototype qualification to full container loads). Standard production cycles typically range from 2 to 4 weeks depending on customized slitting and dimensional specifications.
Q5: Can DLX provide custom coil ID/OD and edge treatments for automated bellows lines?
A5: Yes. We customize coil inside diameters (e.g., 200mm, 300mm, 400mm, 508mm), coil weights, and outer diameters according to your decoiler specifications. We also offer deburred or fully rounded edges to prevent edge tearing during continuous tube welding and convolution stamping.